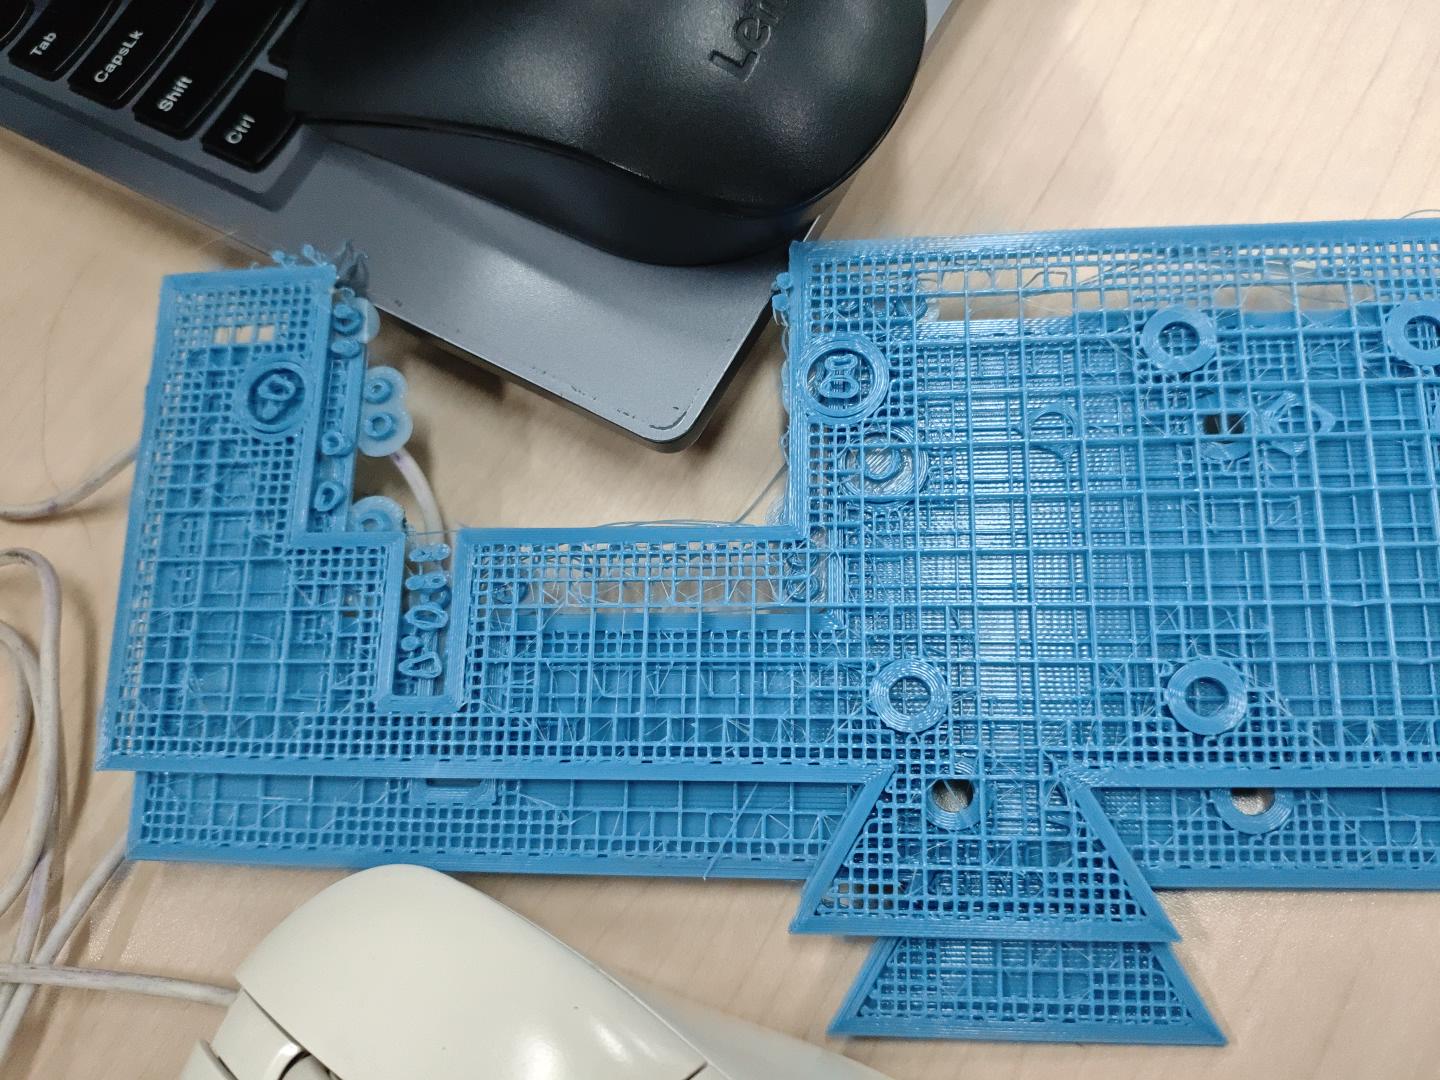
I ran into a massive layer shift issue mid-print, and it’s the first time I’ve ever experienced something this severe. As you can see in the photo, the print shifted significantly along one axis while laying down the infill, completely offsetting the rest of the structure.
Print details:
Printer: K1C
Filament: PLA+
Print speed: 60mm/s
Before this, prints were coming out fine. What could be the most likely cause for such a drastic slip? Could it be a loose belt, a stepper motor driver overheating, the nozzle hitting the infill (grid infill catching), or something mechanical?
Any advice on where to start troubleshooting would be greatly appreciated. Thanks in advance!
if you want to make sure, that it’s not a loose bolt on a stepper motor, just make some test print, pause it and try to move the printhead in all possible directions….obviously it will be X/Y axis in this case.
On pause almost all stepper motors will be ‘blocked’ from moving freely. You should not be able to move the printhead, or it should be so hard to move, that the whole printer will slide on a table.
Make sure the belts are not missing any teeth.
Aside from that, i would try different slicing software, maybe it’s just the software.
Also, when you pause the project, the printhead will move to it’s pause position, i would mark that with some white marker or take a photo, and compare the pause position while printing some test project. if the pause position changes, it may help you pinpoint which axis it is.
If some cables delivering power to the stepper motors are broken, and the broken spot get’s into action only at a certain position of the printhead, then you are in for a wild goose chase, as finding it will be fairly impossible without some dedicated equipment to read out the voltage while the printer is printing something…..at least knowing which of the 4 wires is damaged, would help in finding a solution.
On almost all 3D printers, the stepper motors give no feedback at all, so the software ‘assumes’ the printhead is at the correct position.
Each time you start printing, the printhead or bed as well, will calibrate itself by going full way in all possible direction until reaching the end switch, that switch is the reference point, after it has been reached, the software ‘knows’ where the printer head is…..all that assuming the stepper motors are powered 100% of the time and there is not much resistance for the printhead movement.
More advanced printers use cameras for redundancy , there the position can not be lost that easily.
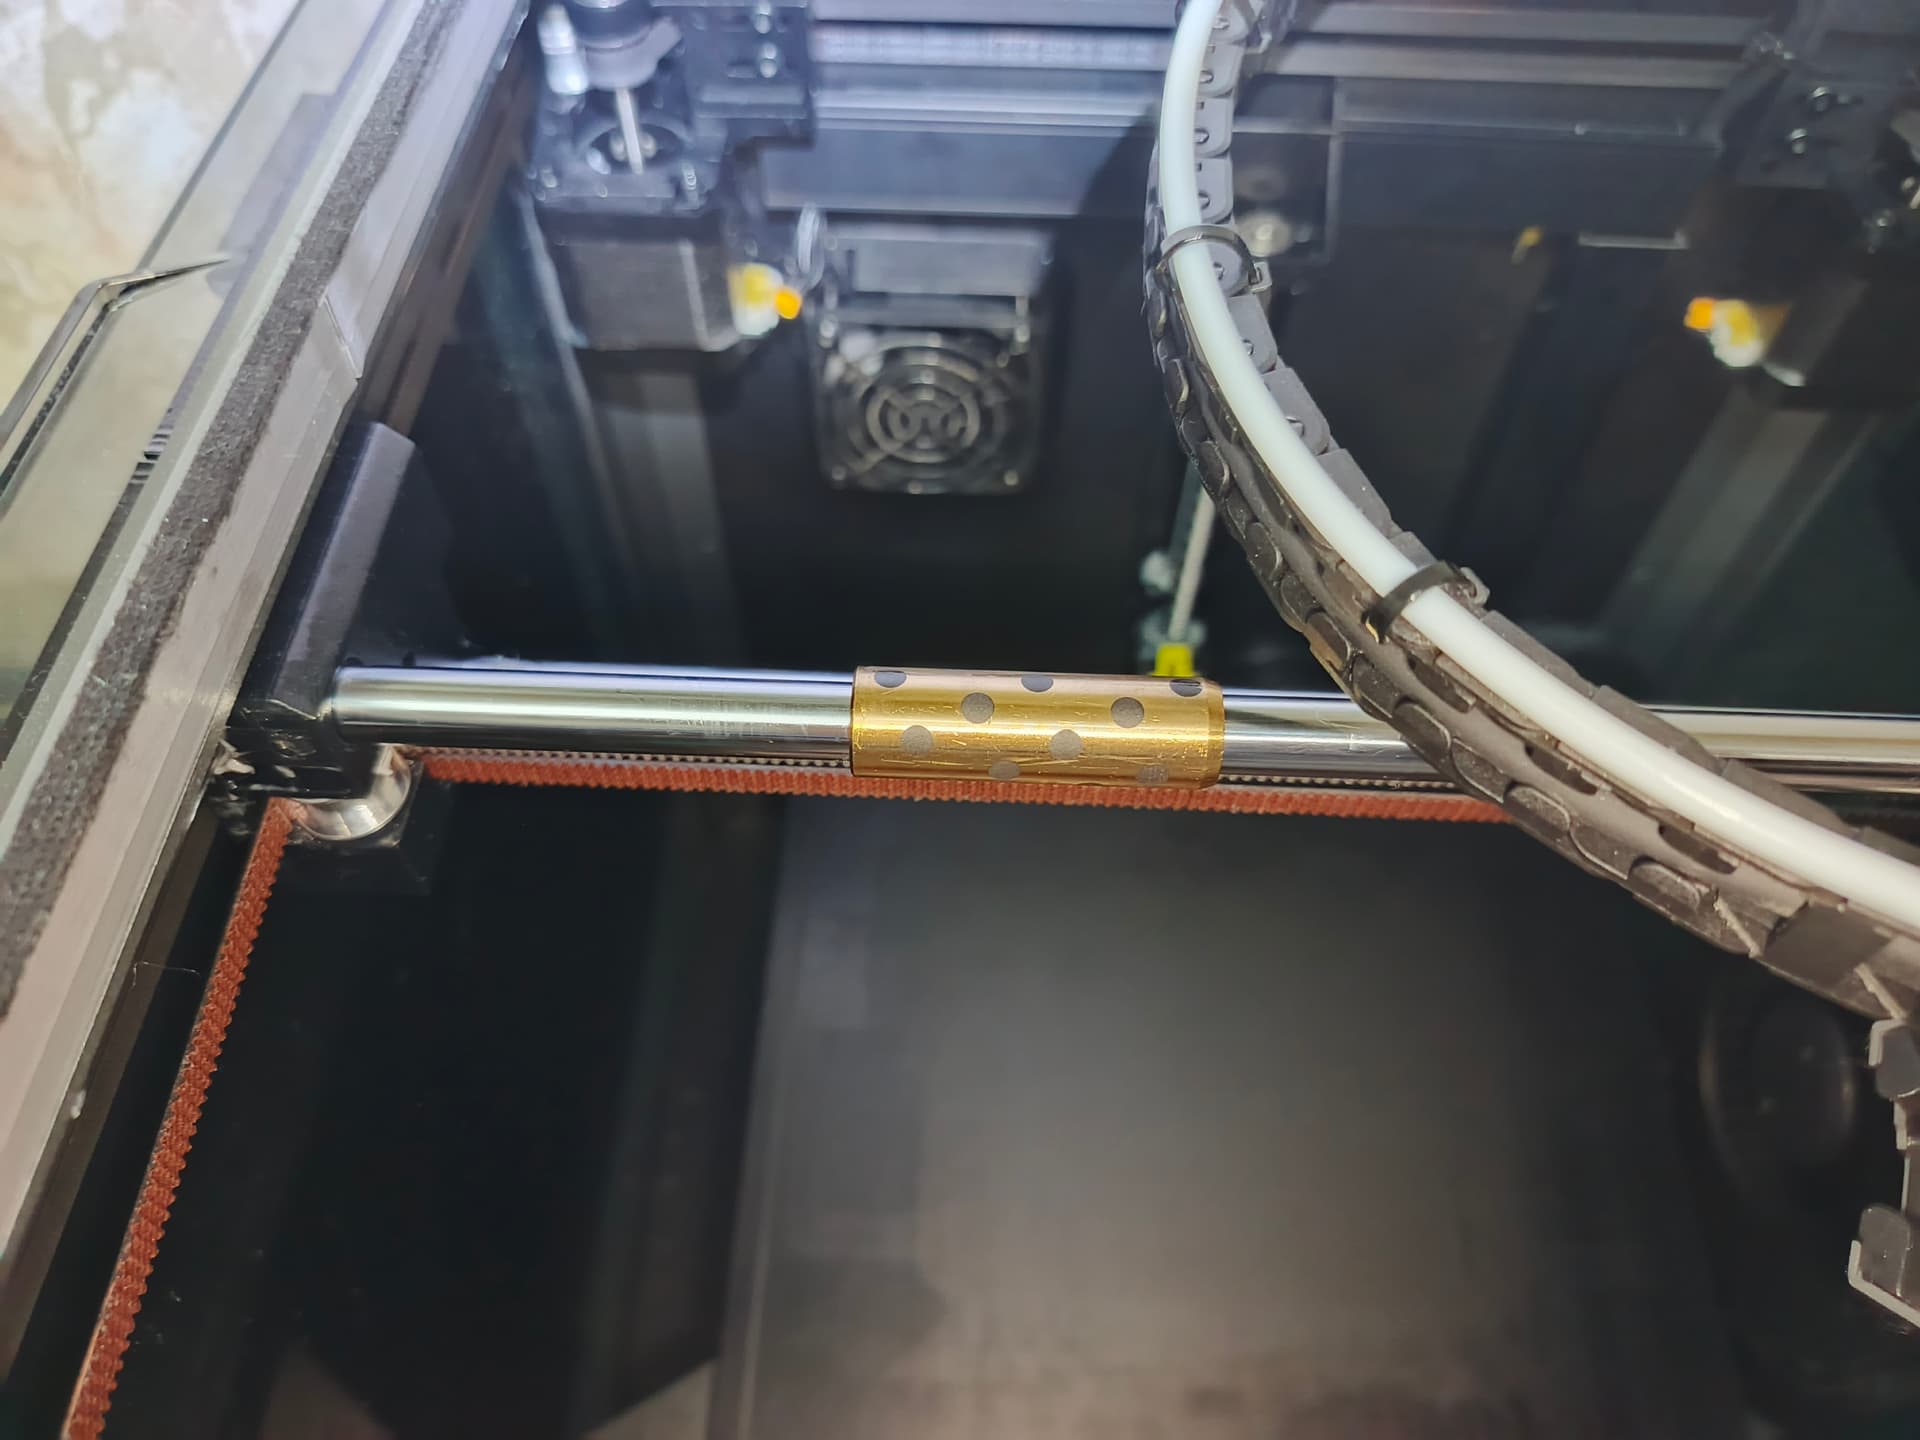
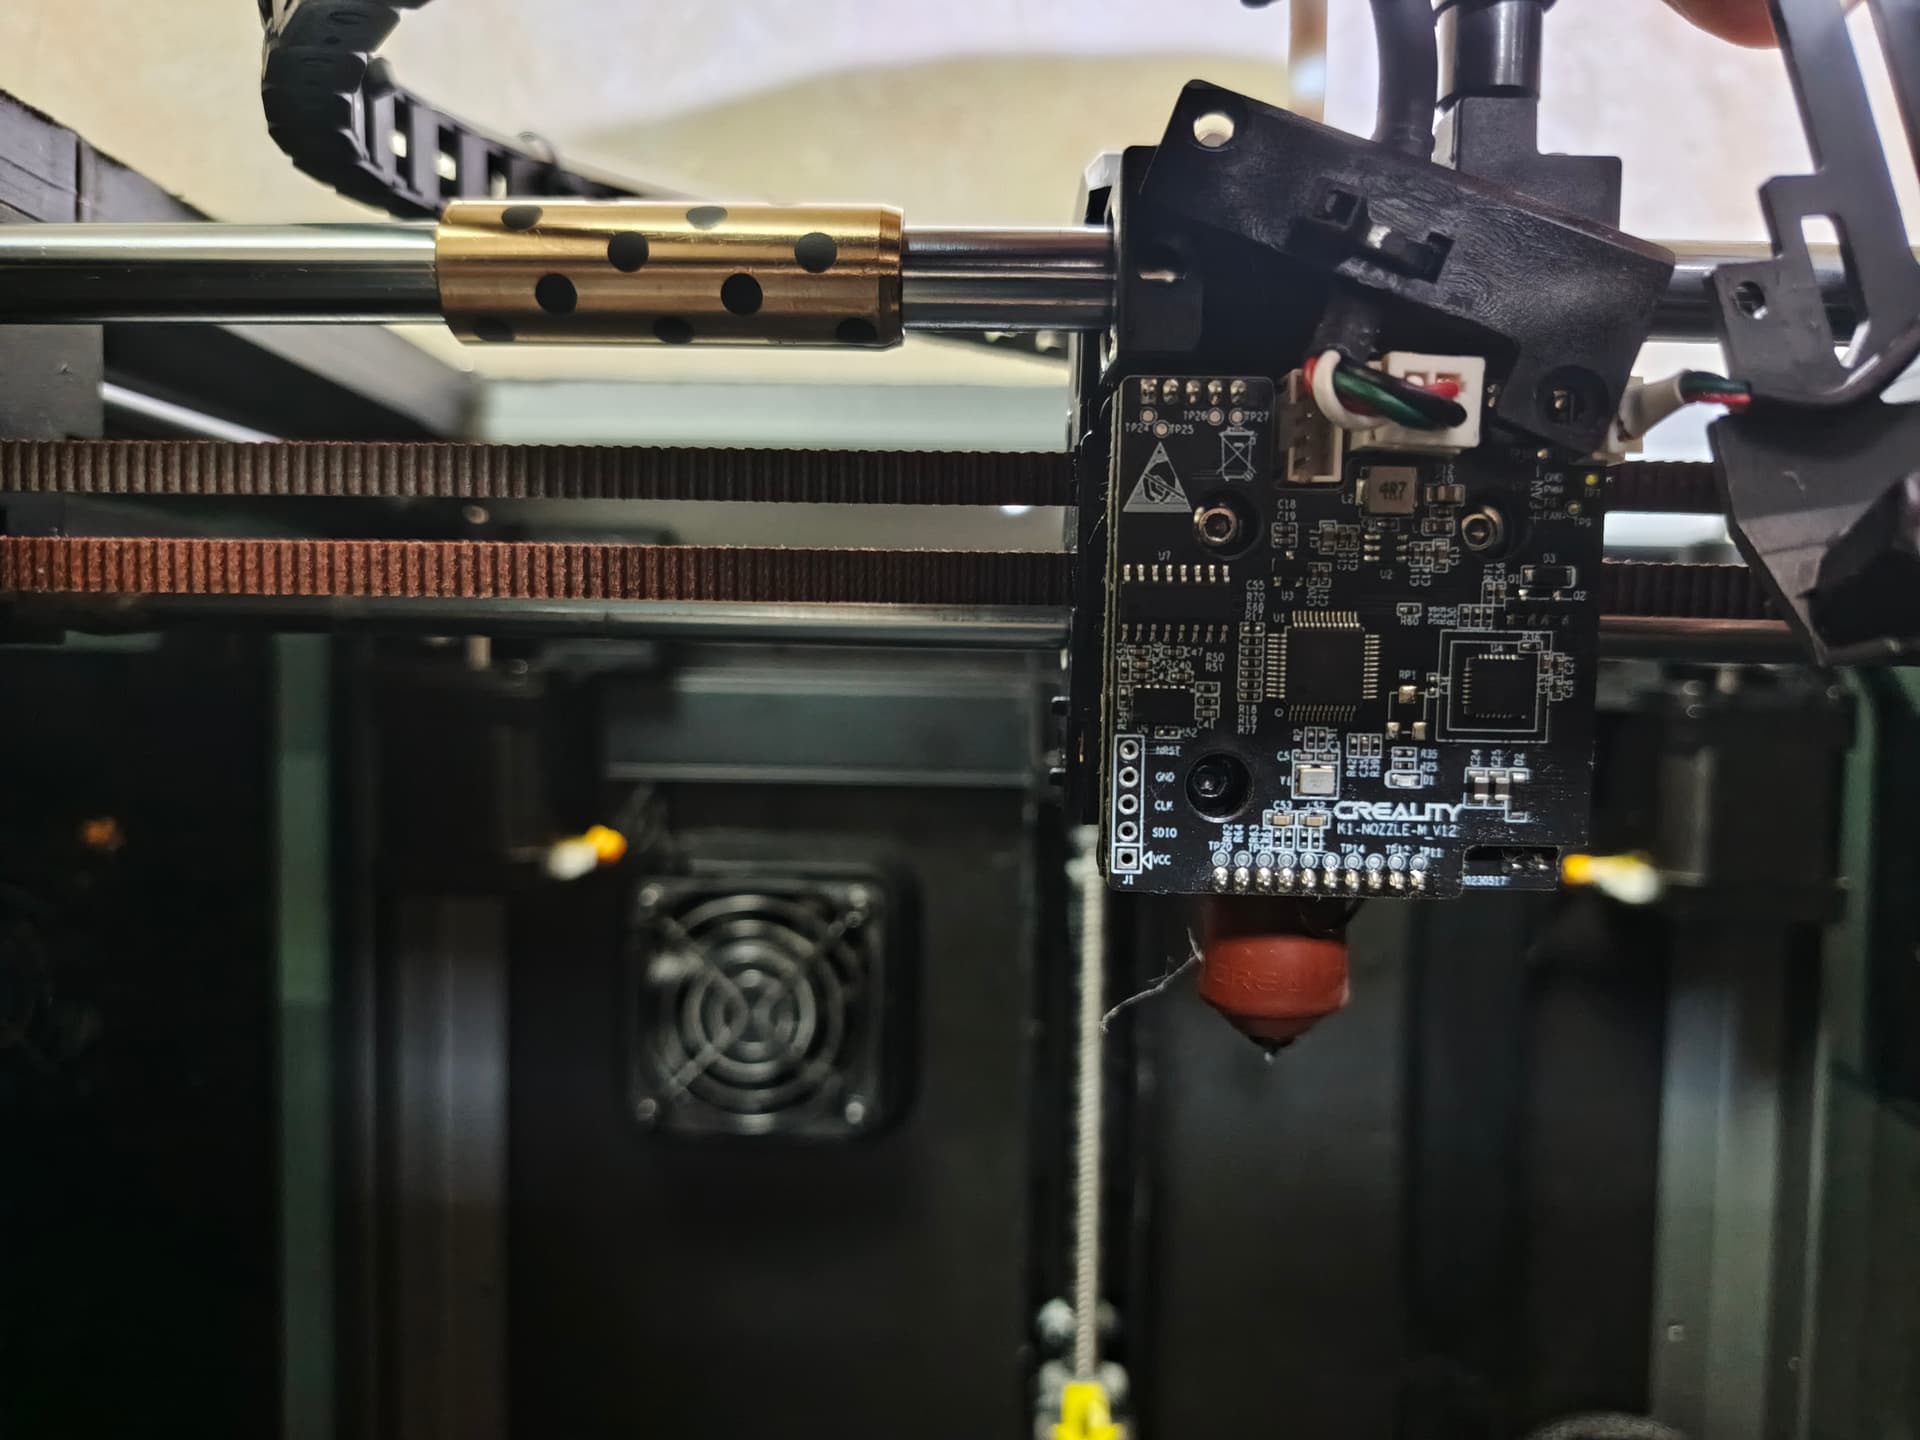
Hello, the layer misalignment issue may be caused by a software error or mechanical failure. Try thoroughly cleaning the X-axis plain bearings, then lubricate them with machine oil. I used weaker bushing pressure springs on my printer to reduce wear and reduce the load on the stepper motors. Layer misalignment may be caused by the print head jamming during movement, which occurs under certain conditions. Start troubleshooting step by step: test models, print at different speeds, clean the plain bearings, check the belt and belt tension, and check the idler pulleys for possible jamming. If you manage to solve the problem, please let me know.
I had the exact same fault but in the last third of big prints ,after a lot of time i found like a poster below it was those graphite bearings .I bought a new set from aliexpress but take plenty of pictures theres a lot of dismantling to replace them .I think its pask of 100% clarity about lubrication of those two bearings .i am now using graphite dust but its a messy way and for goodness if your married dont let the mrs see you blowing the stuff around .on a side note dont hoover it either graphite dust is extremely dangerous around electric motors i hold a damp rag under the tube then tap the surplus onto it ,it really just needs a minute layer to work
@user5288579351
….actually, these bearings are self lubricating, they like to run dry / no external lubricants at all. Brass/graphite on it’s own are low friction components, introducing external lubricants increases friction and enables the external lubricant to catch stuff like dust, which keeps on collecting and eventually damages the bearing itself or even the shaft.
In i 3D printer, there is plastic debris flying around, instead of lubricating the bearings, i would suggest to invest is some high flow active air filter module.
Curious, which filaments are you using the most? I seem to not noticed a lot of dust/debris when printing with ABS/ASA.
Mostly glass reinforced asa .i discovered the bearings were shot by pushing them out and pushing them along the rail ,in a certain bit i realised the bearing had turned and it became obvious there was wear .They are only held in by a screw and i guess when the whole hotend became warm enough the bearings were turning .As i said only in a couple of positions 80% of the time the hotend moved freely .I also moticed as the hotend was going to shift one motor got very hot ,i guess it was having trouble moving the hot end .A set of bearings from Aliexpress and the problem went