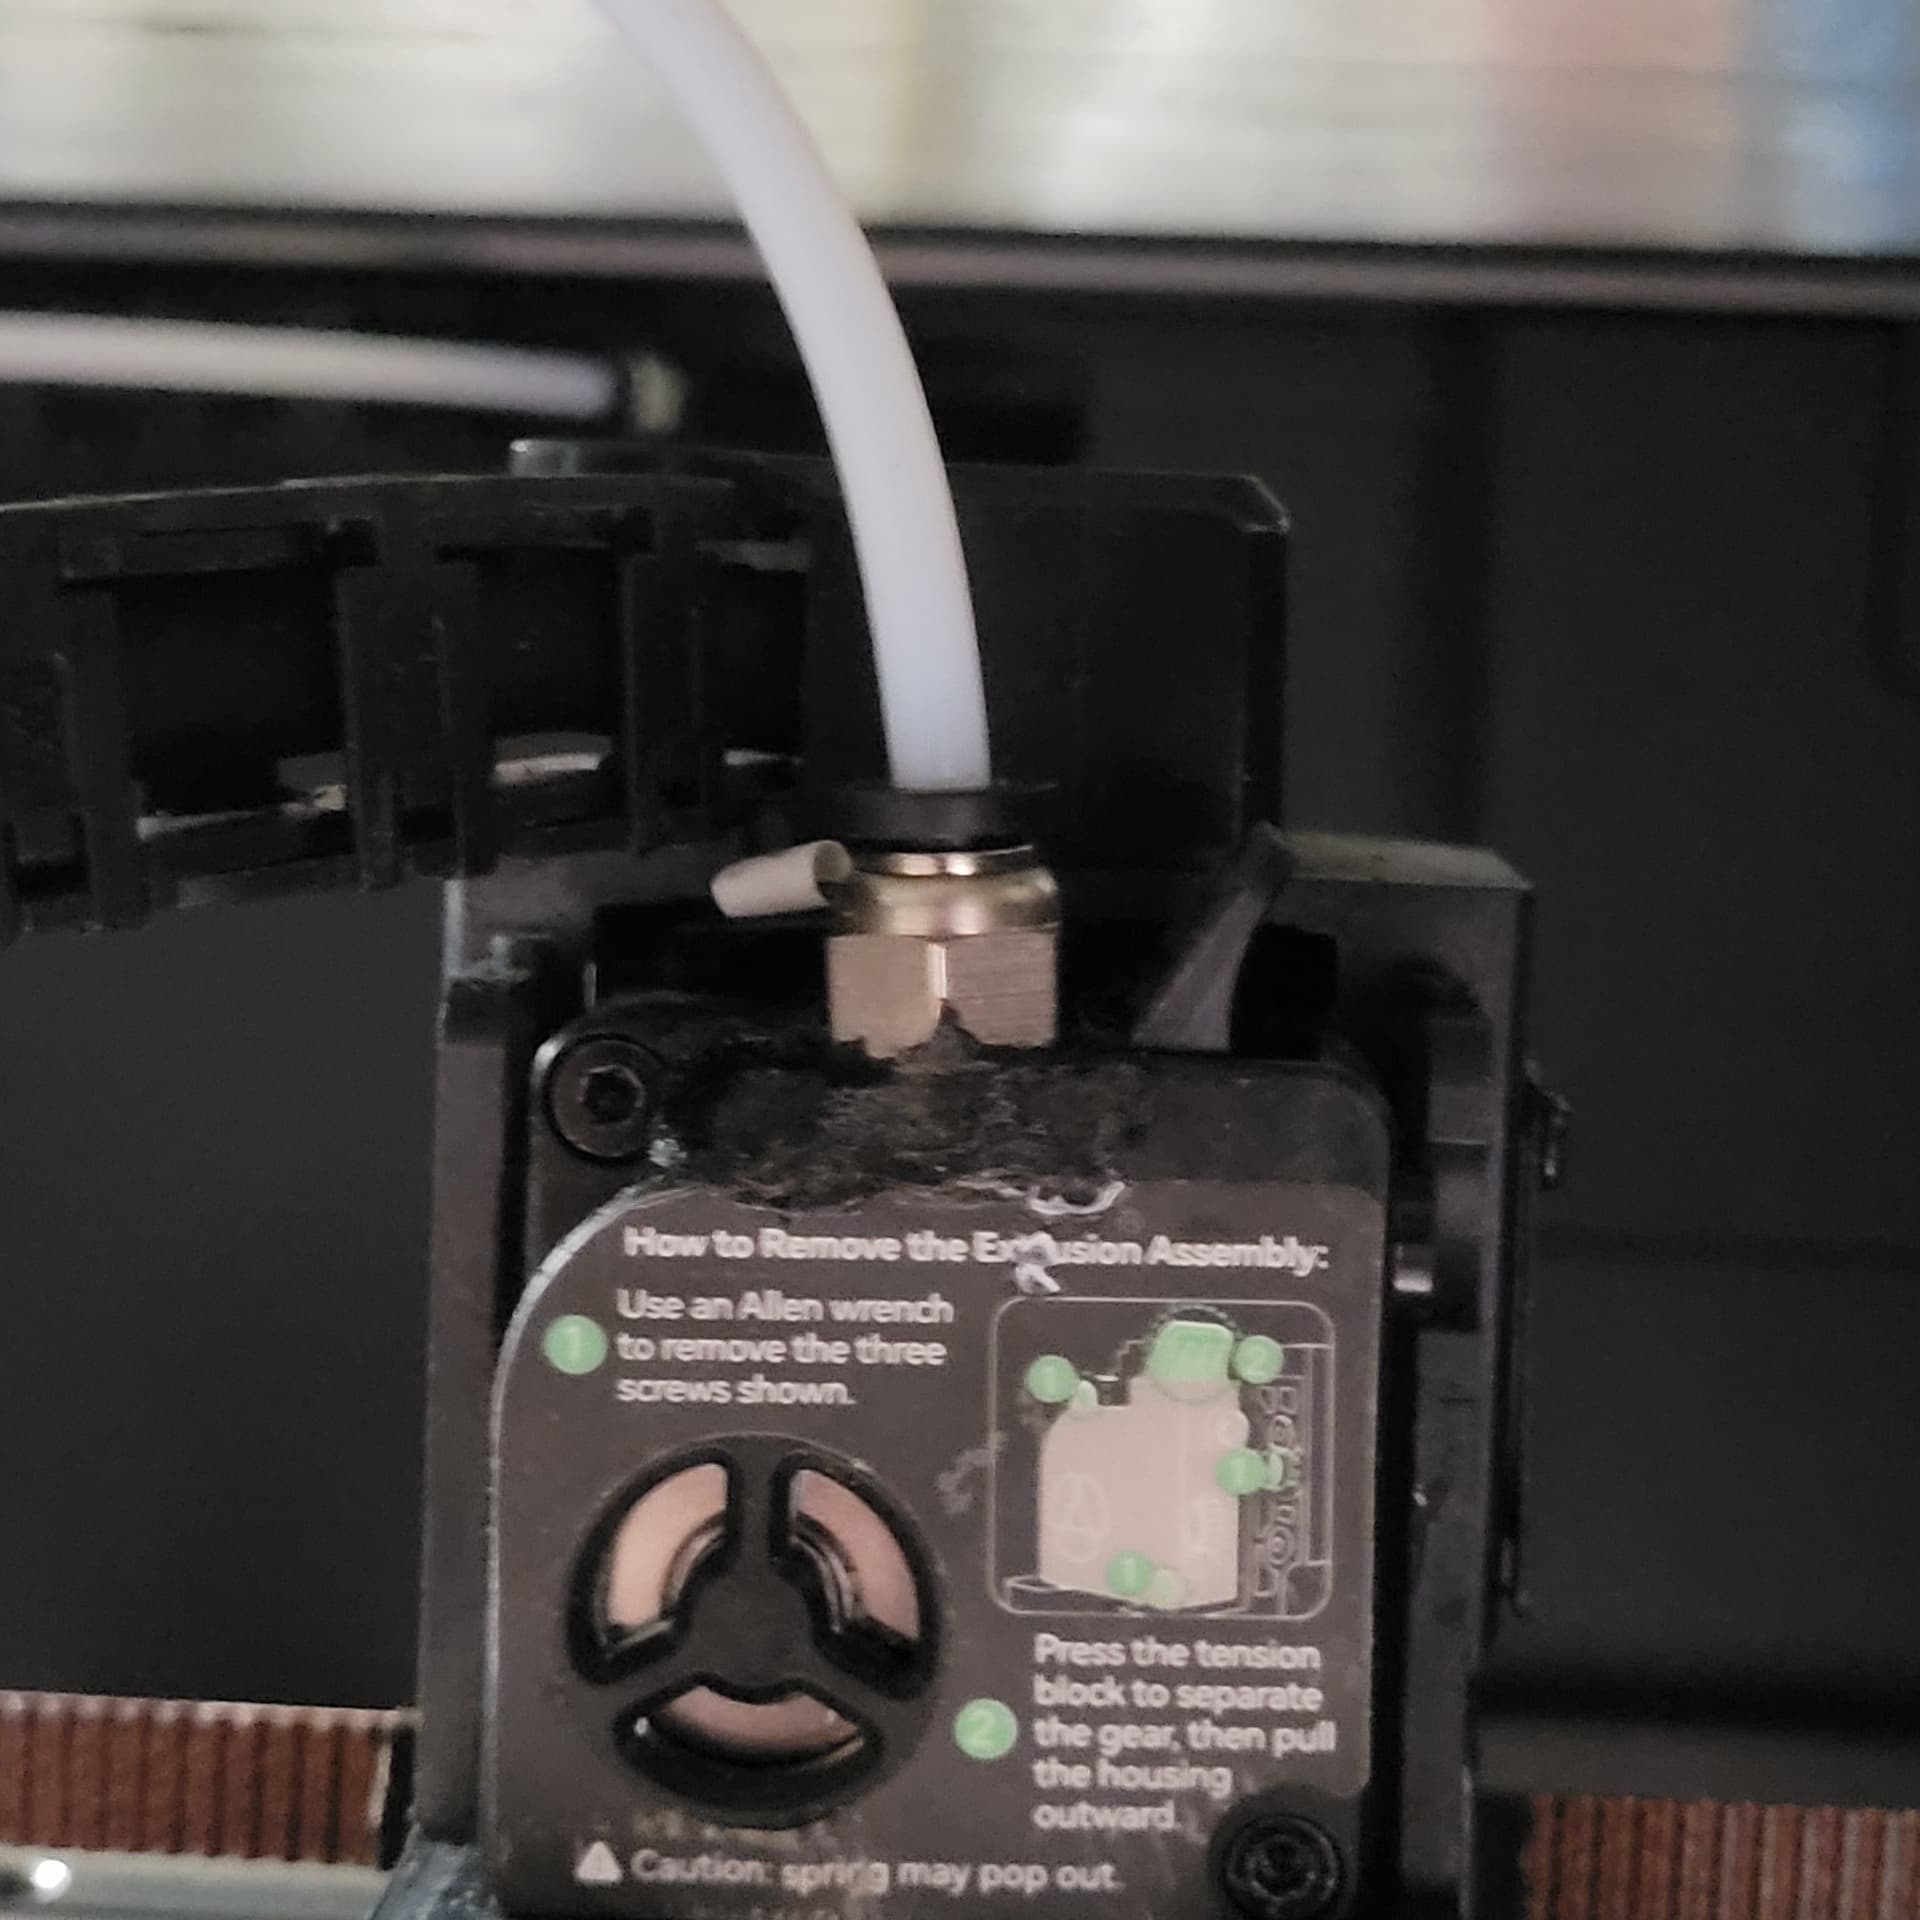
I had to strip my extruder down for the first time this week and i have been printing ok since putting back together apart from the PTFE tube keeps coming out.
What have i done wrong ?
I had to strip my extruder down for the first time this week and i have been printing ok since putting back together apart from the PTFE tube keeps coming out.
What have i done wrong ?
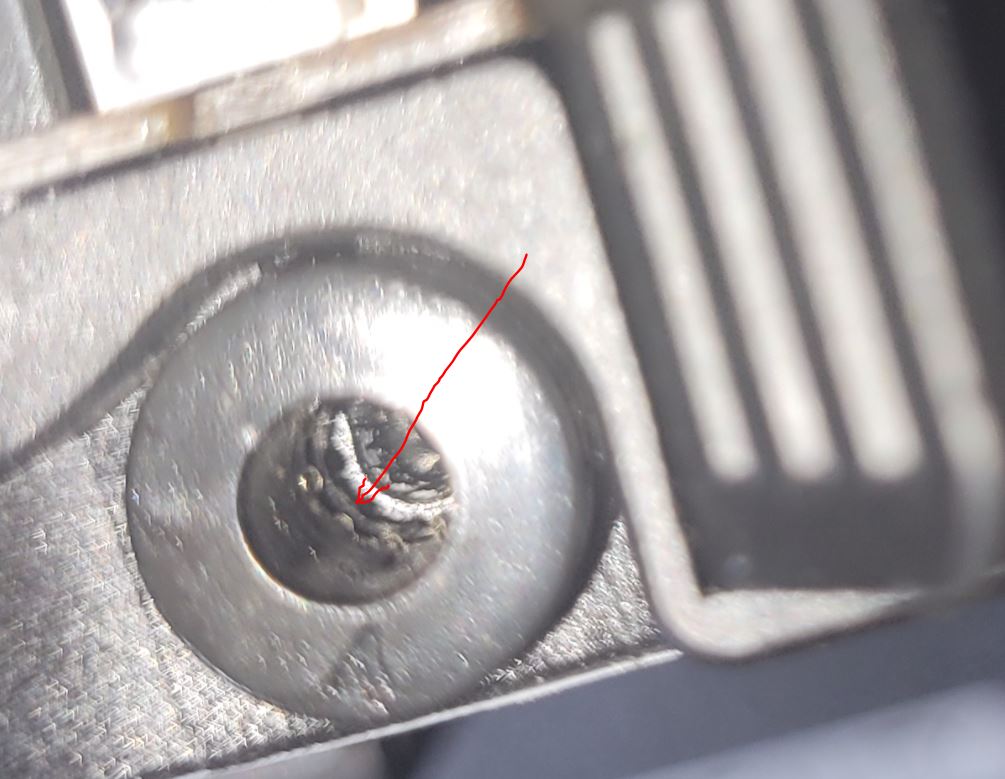
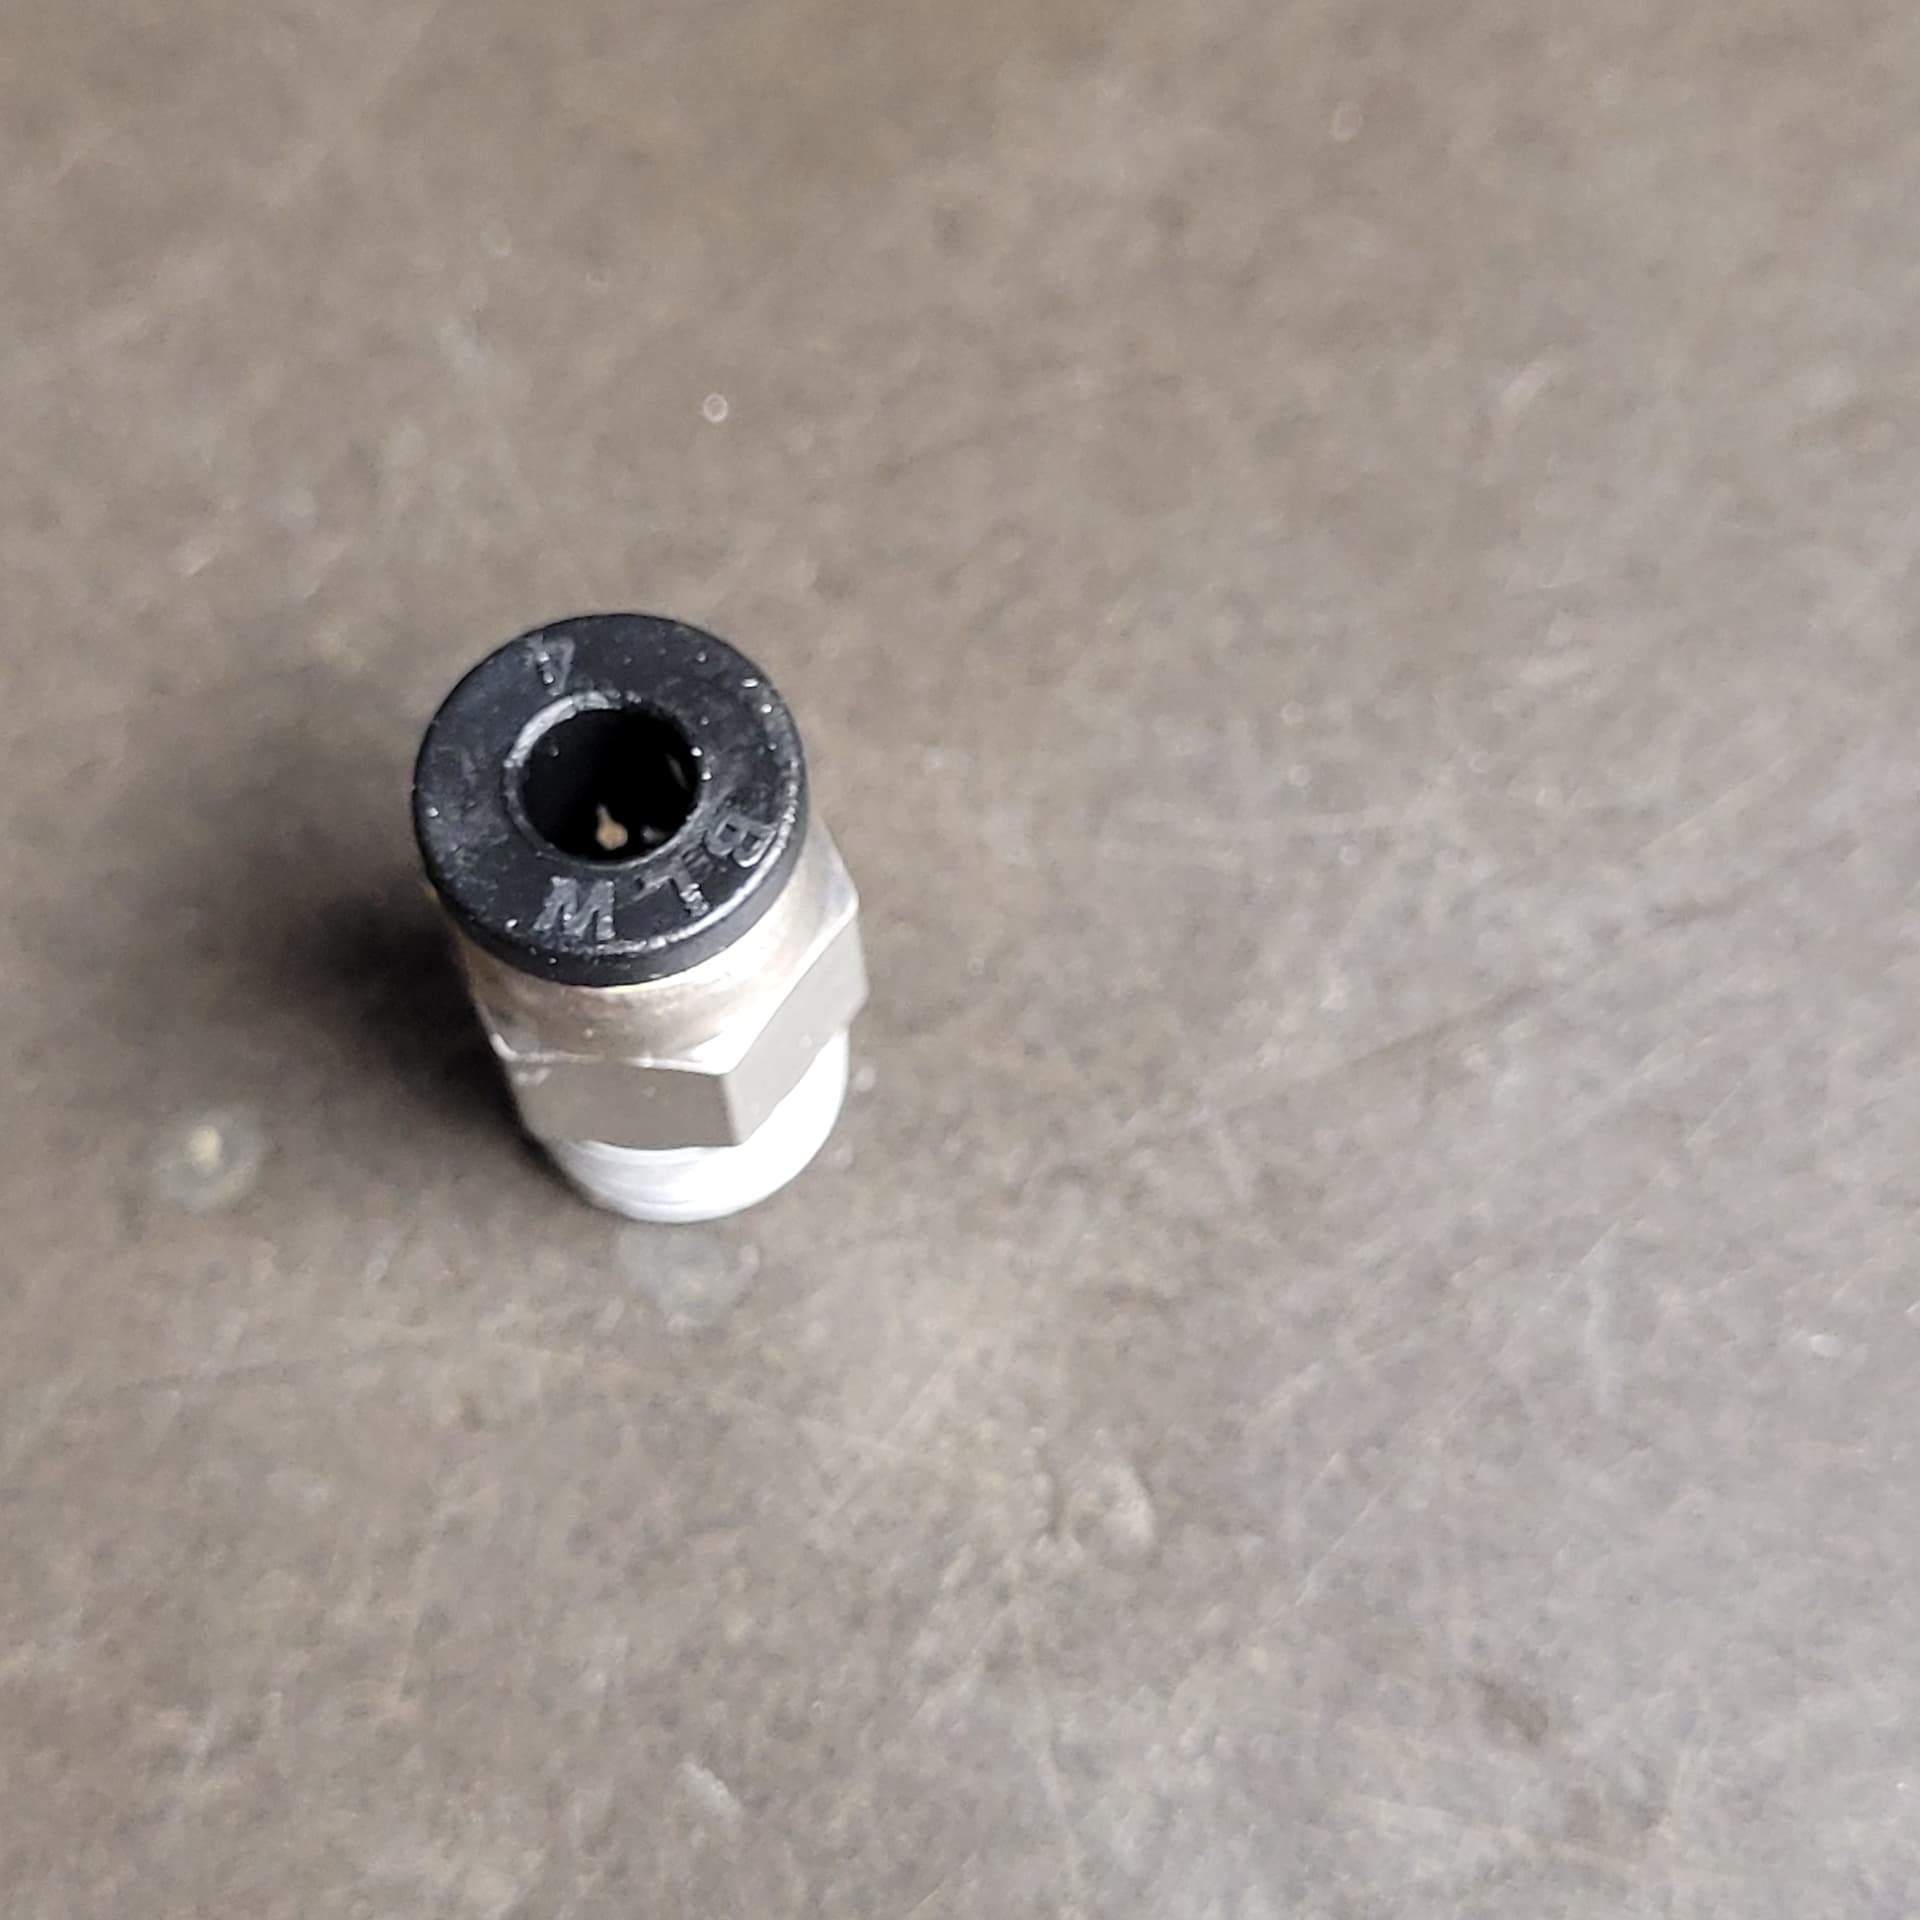
If you have pushed it in as far as it will reasonably go I do not think you have done anything wrong. I think you may have symptoms of a known problem and may need to do some hunting. The black fitting that the PTFE tube goes into has tiny little metal “teeth” in a ring all around the inside. They point in and down to catch and hold the PTFE tube. The red arrow shows one. When you push down the black upper ring (with the 4 on it on my printer) it bends or retracts these teeth away from the tube so you can remove the tube.
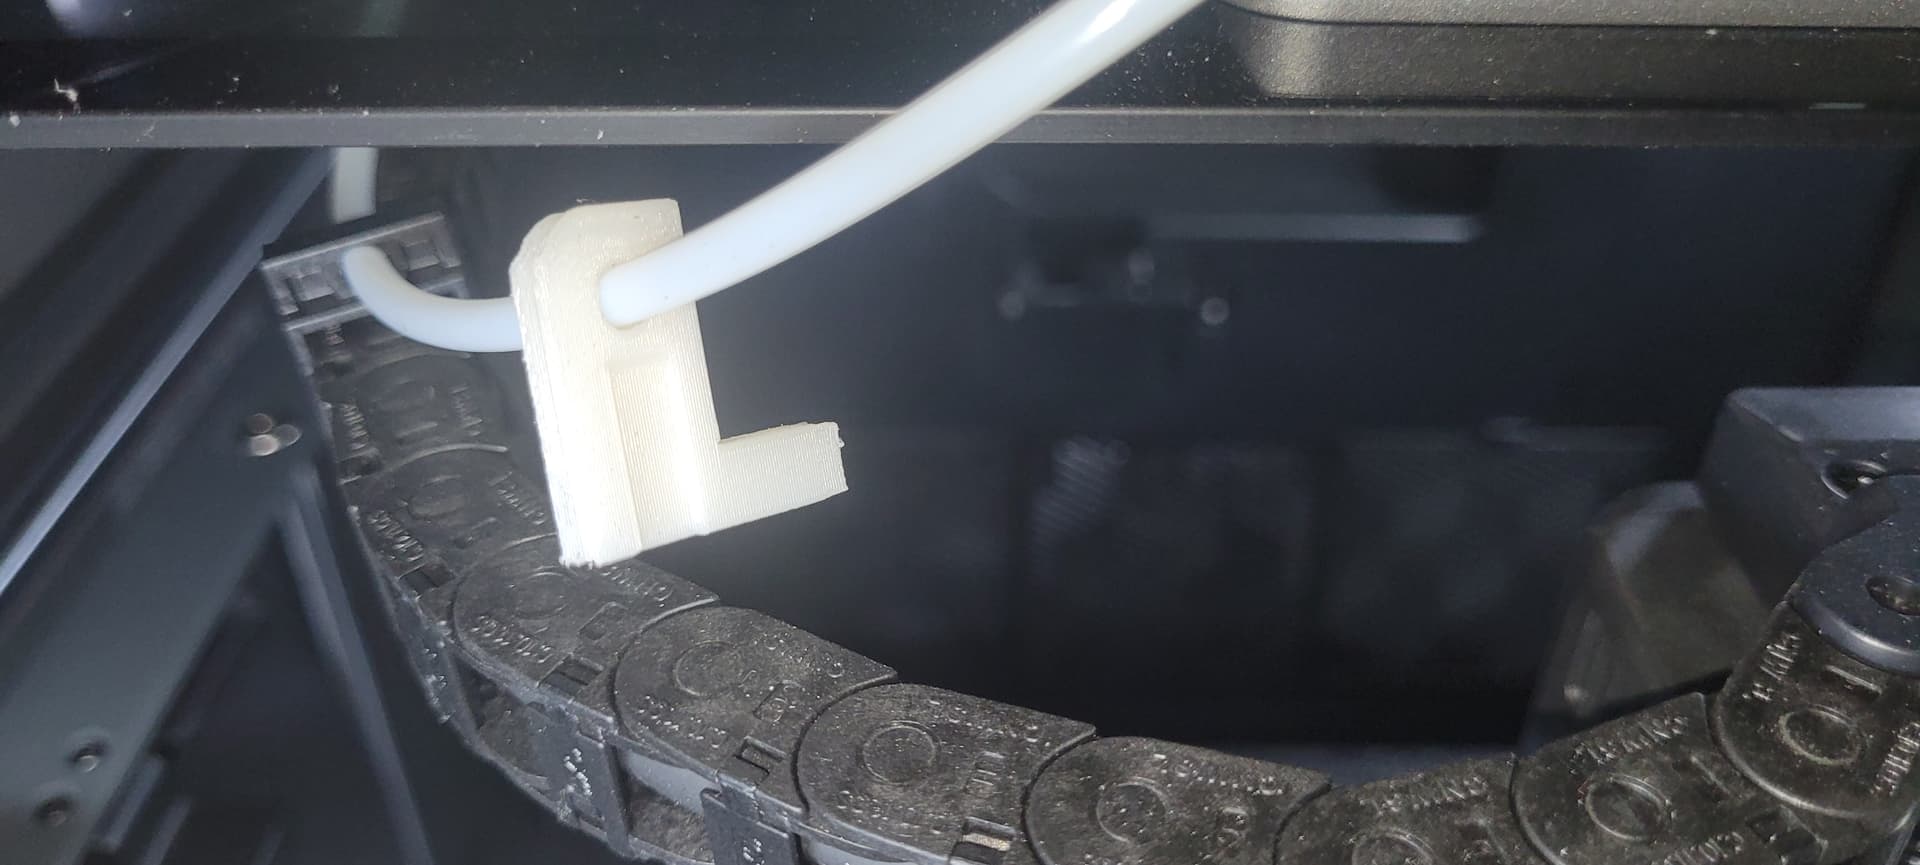
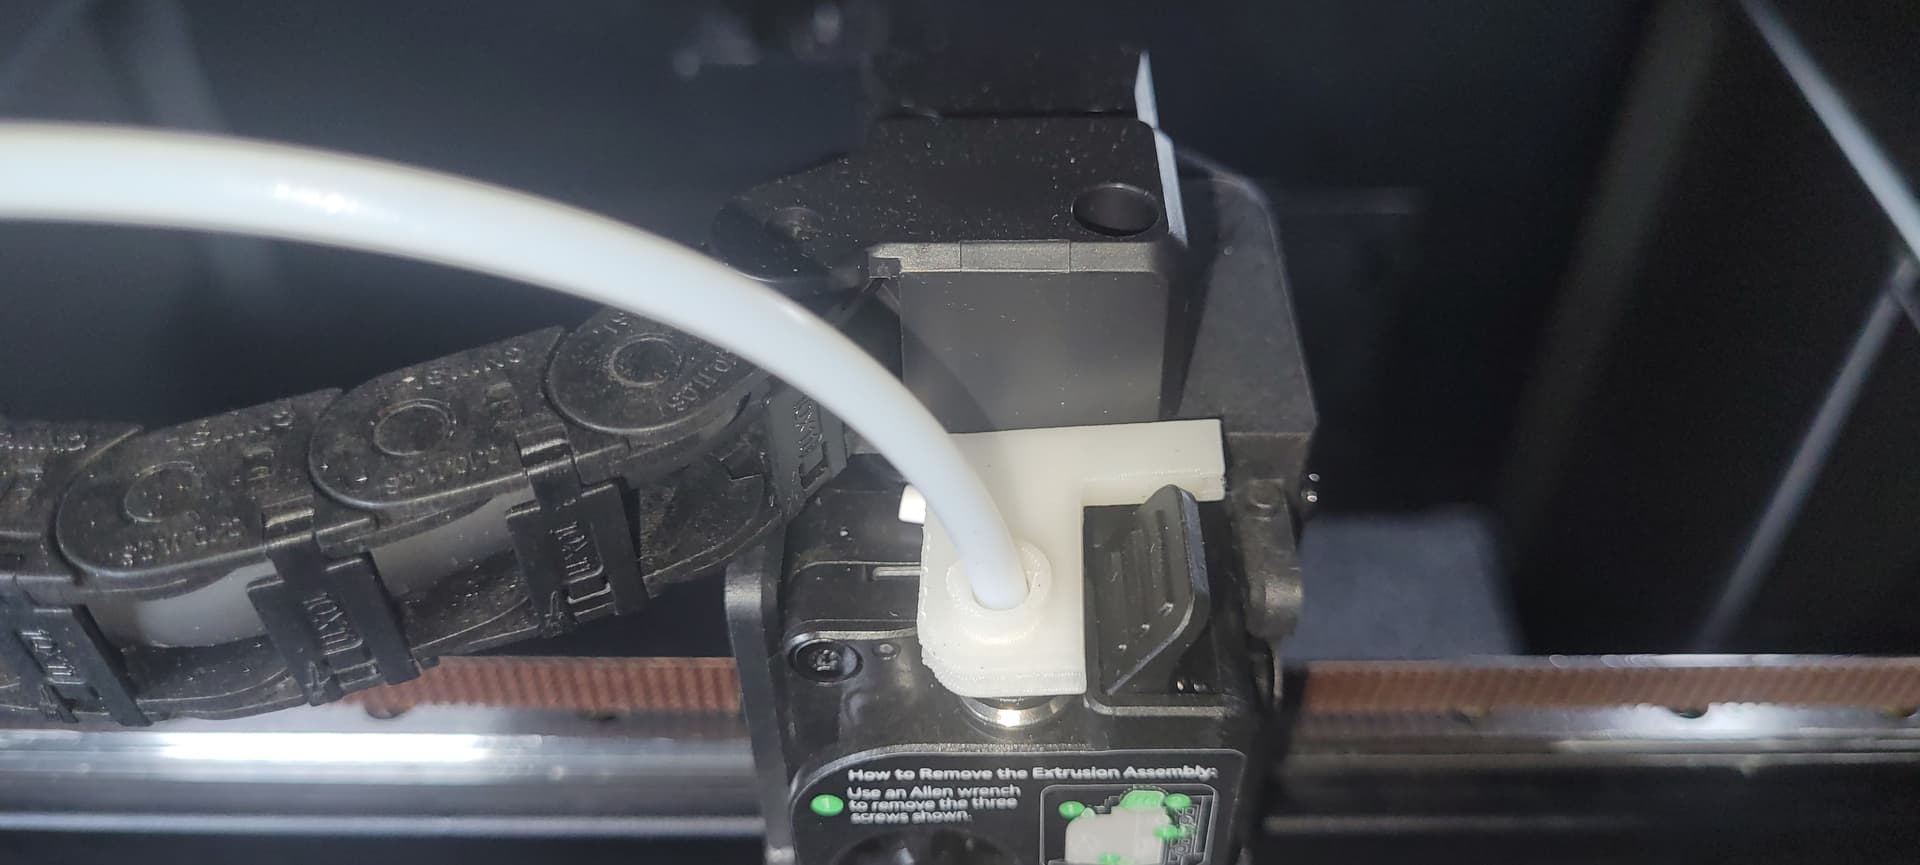
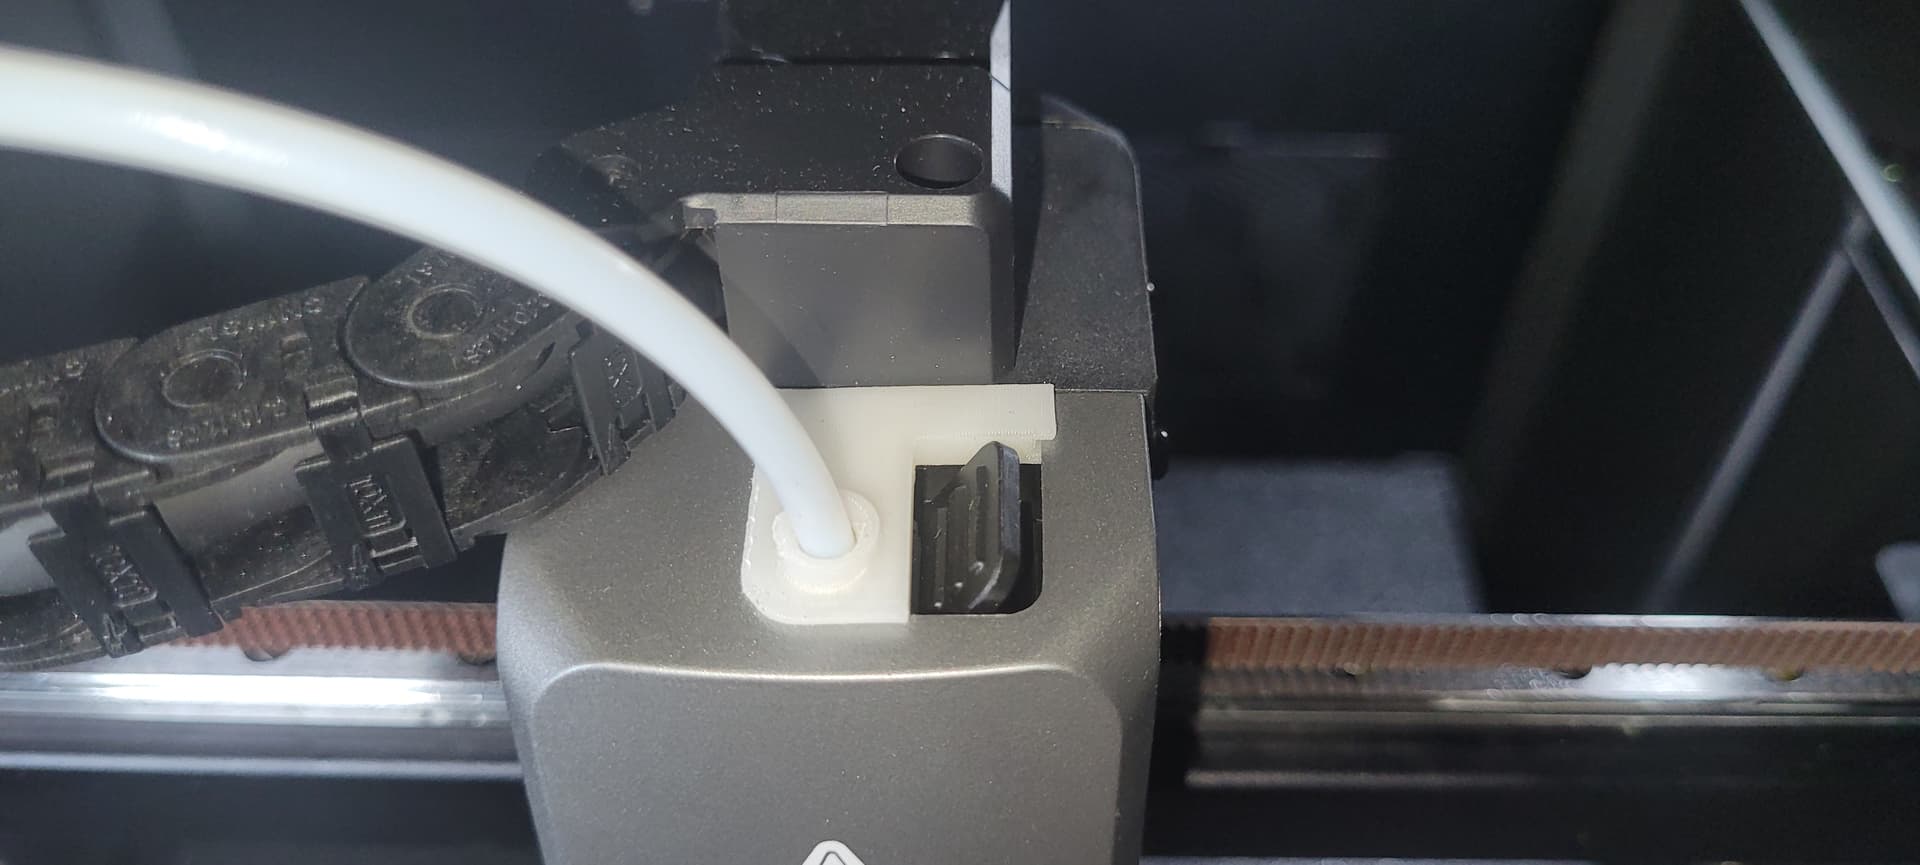
This ring of teeth is known to break apart and scatter bits of spring steel in extruder on occasion. This can cause jams and other forms of carnage. There are a number of fixes that involve printing new attachments for new pneumatic fittings to hold the tube. I printed some as spares and then used the device pictured in an attempt to protect the installed fitting from damage
Thank you for the very detailed reply, i will take a look at this.
Seconded. I’ve just had this problem but fortunately I already had a spare extruder housing sent by Creality from a previous complaint.
I say “this problem”, but I think I’ve been lucky. The teeth just seem to have stoped working rather than disintegrated. I note the end of the PTFE tube that enters the extruder was dark, almost burnt-looking, and deformed, pinched into an “hourglass” type shape at the end. Once I started getting the error that it had detached, it simply wouldn’t stay in the hole. I’ve taken some 6-8mm off the end with my side snips then spent some time making sure the hole is completely round.
Are the pneumatic fittings supposed to be replaceable? As I said I replaced my entire housing, but if it happens again surely there’s a way to replace just this fitting…?
Anyone?
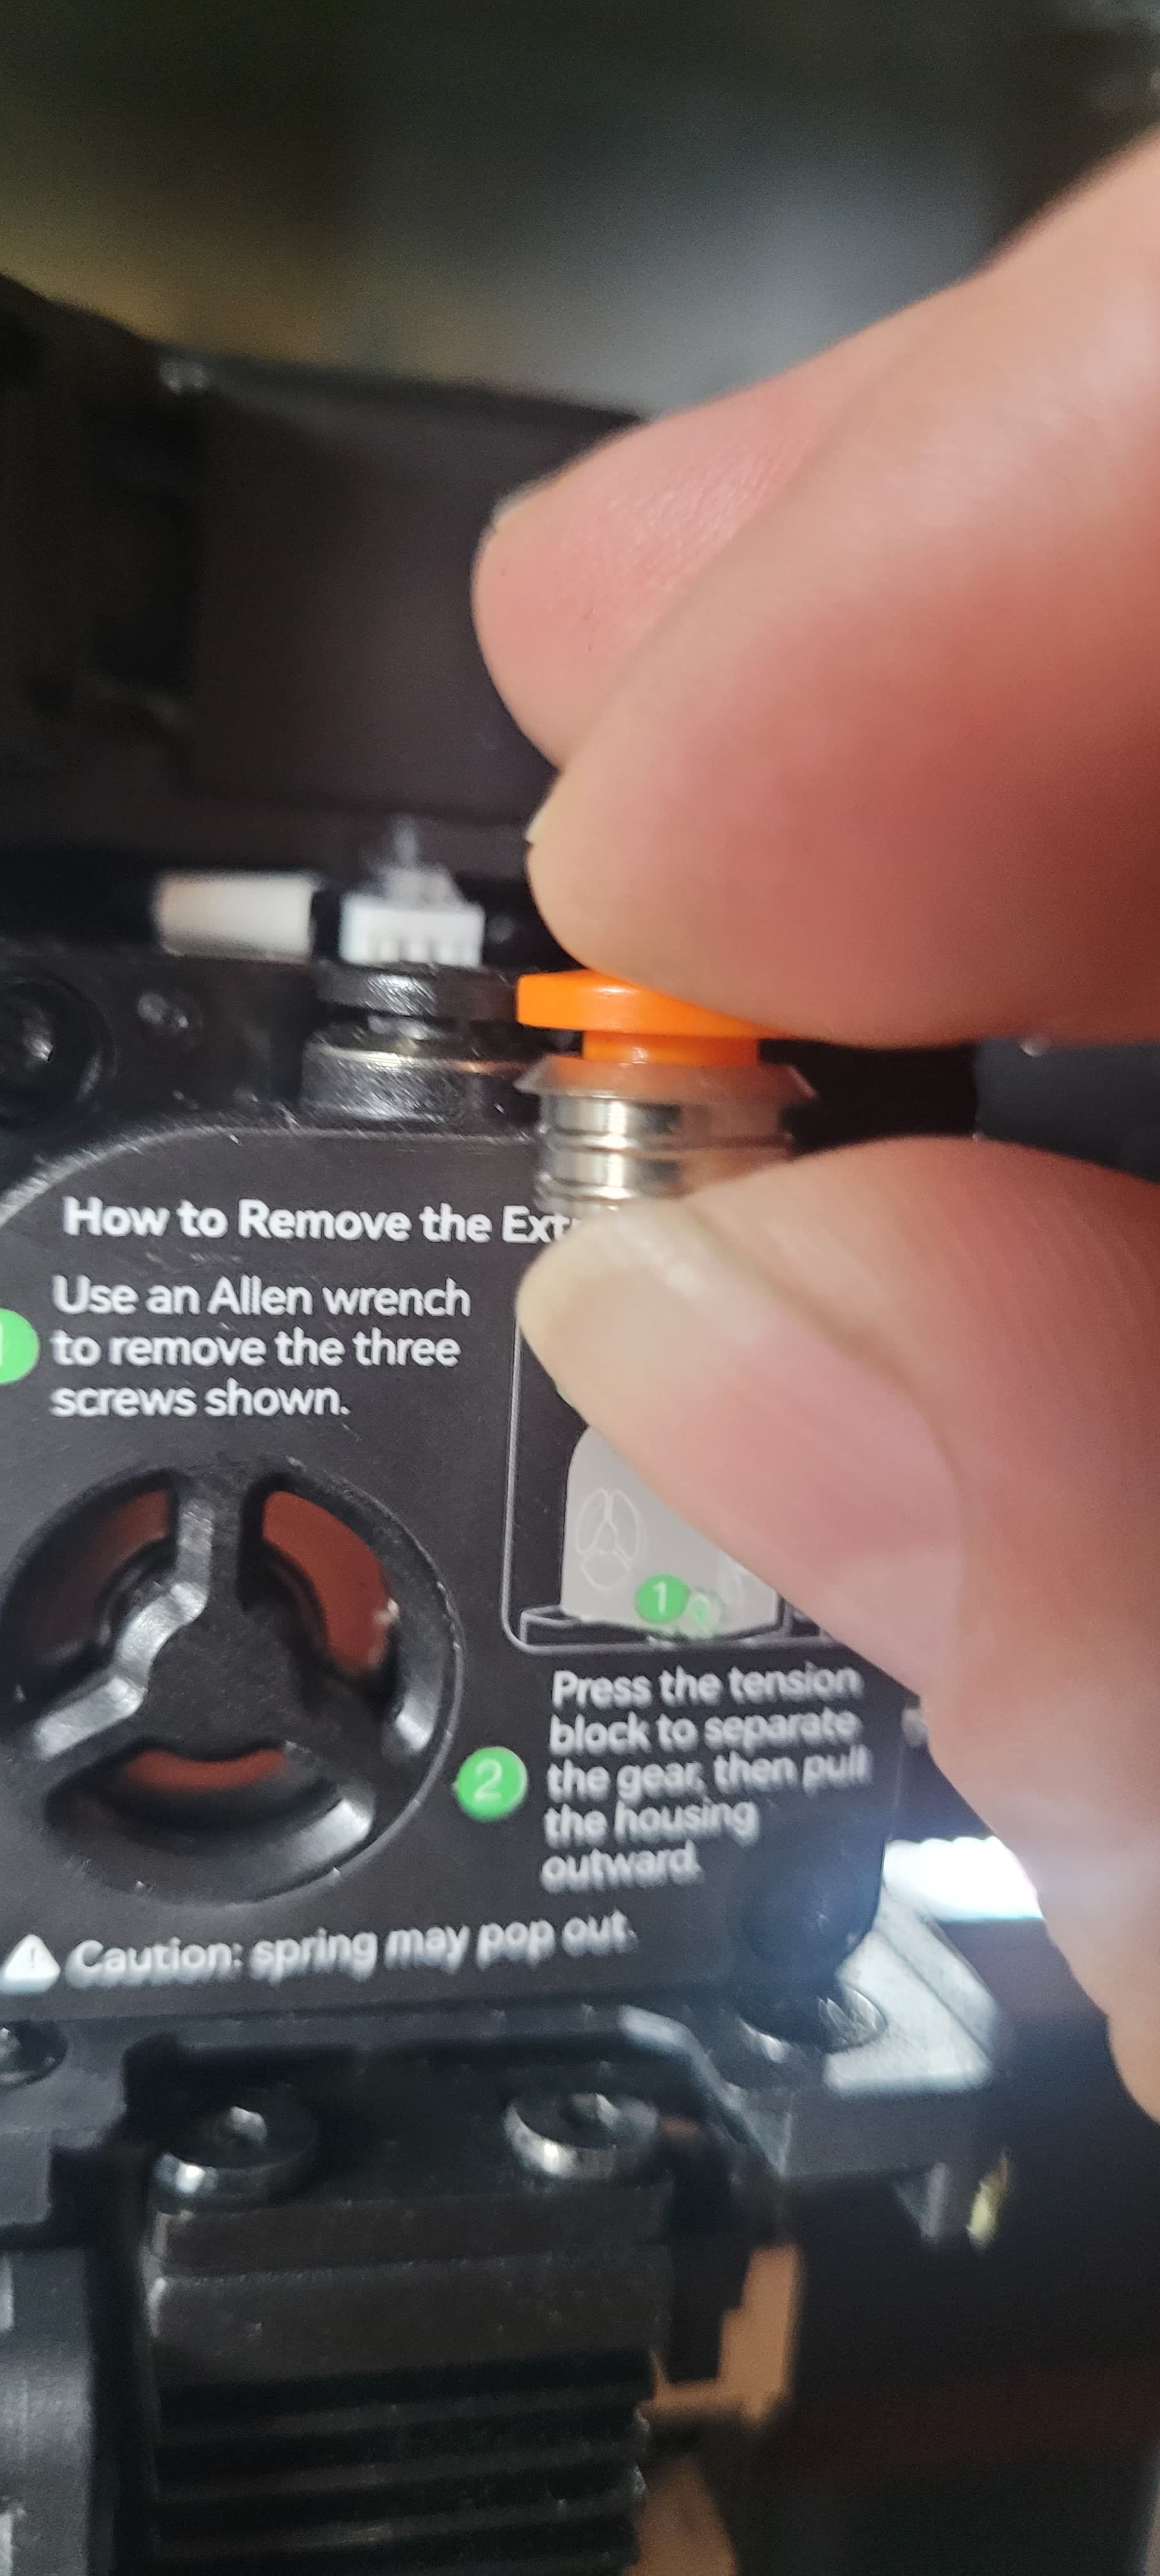
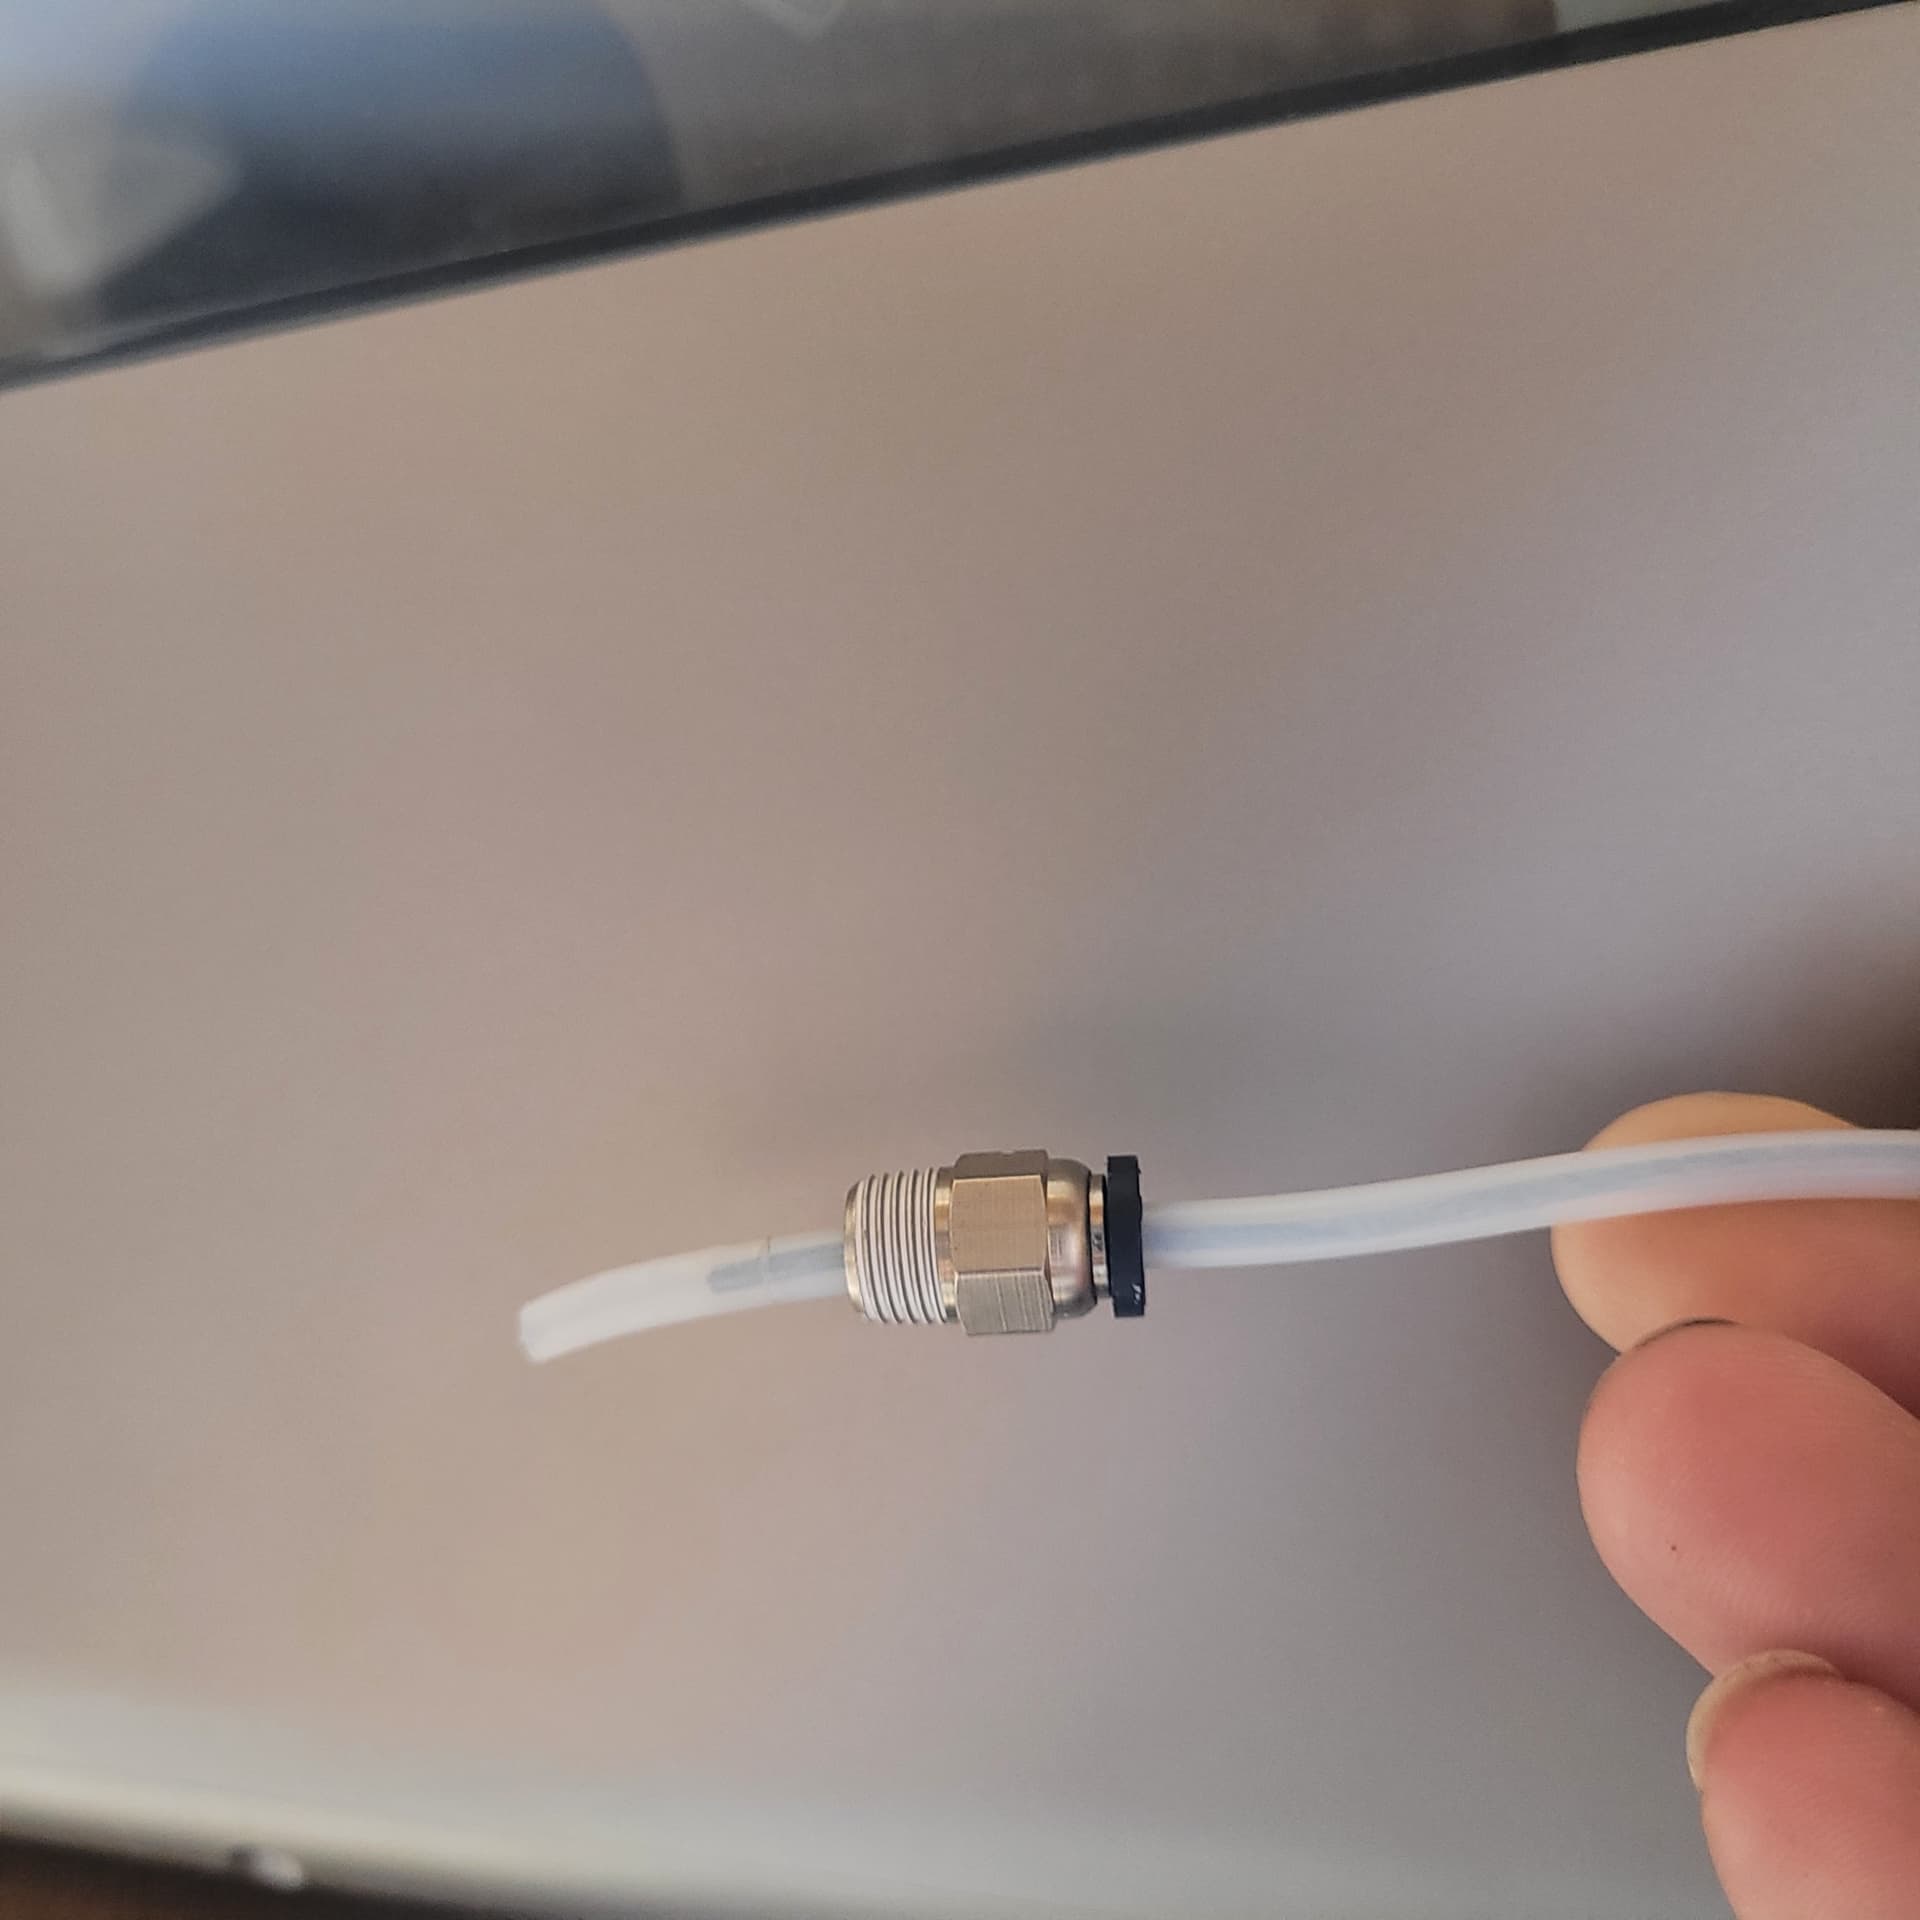
GreyArea, thank you so much for getting me off my a$$ to actually have a look at the condition of the tube end and giving it a needed circumcision with the pictured tool that guarantees a perpendicular cut.
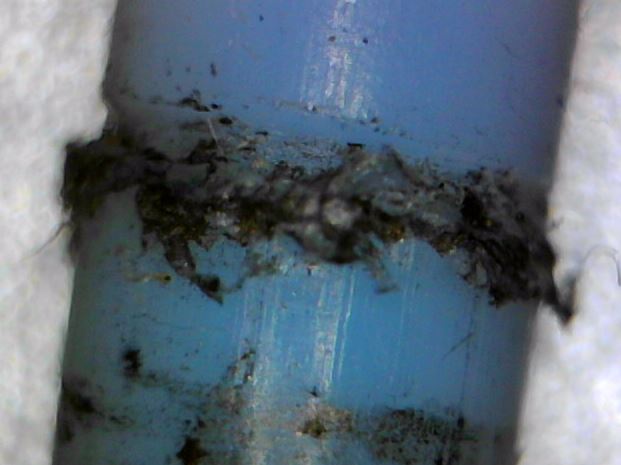
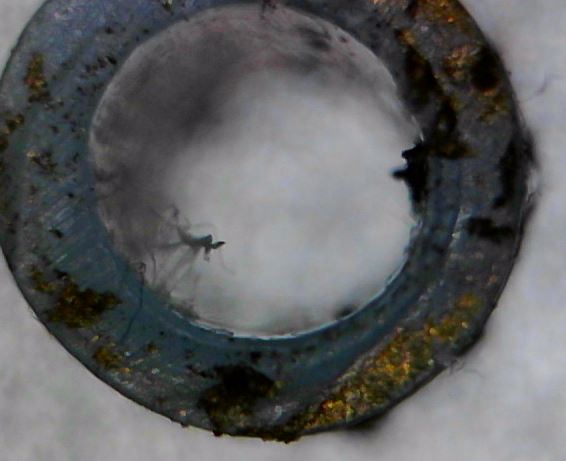
Getting it under my microscope it is not burnt it is almost worn through and that is NOT a lot of printing in my book. Even with a strain relief that attachment is a high wear and maintenance point. I would like to ask Creality to put configurable maintenance alarms in for this type of stuff.
Now to that fitting. Spring steel against a PTFE tube, we all know who is going to win that battle. Wiggle it about, push it against the upper glass and you have the basic design of a vibratory saw. A recipe for rapid wear. I believe the fitting is cast into the housing. I did buy some similar fittings but not having a spare housing, I do not want to sacrifice it until I have to.
I don’t know a lot of “stuff”…but I ask good questions, no?
I’ll take the pat on the back for starting this one, @Cannonman will do most (all!) of the work, so the applause is his!
Did I start this one ??? 
LOL to be fair, you did, but I think it was my comment about the state of the end of my PTFE tube that got @Cannonman’s gears whirring.
I’ll split it with you…one pat each?
Just to finish off this thread Creality have upgraded this part ( there is a message from creality about this on this forum ) Creality did send me a replacement part and this has fixed this issue.
Can you shed some light on where to find that message from creality about a upgraded part? I had a Extruder fail due to the gears, and they sent me a new one, now 2 months later my tube pops off mid 20 hr print and will not stay in no matter what I do. Now trying to figure how to not waste a ton of filament by having to scrap this print and start over. I put a support ticket in today but in my experience a replacement part is weeks away.
Could you share the STL file for the part you created to mount the PTFE tube to the print head?
So, I went through a few designs and not one of them really solved the issue. The solutions would raise where the bend on the tube occurred and the tube would hit the top glass. I reworked my existing extruder and bought a spare one. I now have over 1400 hours of actual printing on the unit. Here is how I got there and some watch outs for your unit.
1- Remove the cover on the front of the extruder. Most of the “fixes” involve modifying or attaching something to it and I run straight out of the extruder fitting. One of the lower plastic screws the magnets of the cover sticks to pulled out for no reason. I replaced both the screws with a much longer machine screws. These hold the lower air nozzles next to the hot end.
2- Pull out the PTFE tube from the extruder every 200 hours, inspect the small metal fingers or teeth that hold it in the fitting, you may need a magnifying glass or jewelers loupe to do this (removing the extruder makes this MUCH easier. If the teeth are ok, cut off ~3/8” of the damaged end of the PTFE tube and reinstall. PULL on it to make sure it is properly held by the extruder
3- Every 500 hours install a new extruder OR CAREFULLY heat and pull out the stock PTFE tube insert and replace it with an industrial one. The stock insert is known to grenade and dump metal bits into your hot end. Destruction is probable. As a rule would put a new insert in a new extruder because of this.
4- Every 1000 hours install new extruder drive gear/teeth wheels.
Ramblings:
The textured PEI sheet works well and will print small components from a cold start with zero issues. I print a lot of ABS (90%) and it loves to warp. Lately I have been printing full bed components and the stock bed on the K2 Plus, for full bed prints is junk. As it heats, it twists around like a worm on hot pavement. Once it is hot and stable it is reliable but finding this out through MANY levelings and aluminum foil tape caused me to loose a fair bit of my meager stock of hair. If I have to print a lot more full bed components or tall slender ones I am considering an R3men graphite bed upgrade. Currently printing ~ 20 hours a day so the numbers are racking up.
Nice post on the details @Cannonman. OK, this is a design issue with the extruder. The immediate fix is to replace the Bowden tube connector. The long term fix has been posted and it is a printed bracket that supports the bowden tube reducing stress on it. The Bowden tube also rotates in the connector especially during Y movement. That movement makes the connection more loose eventually to the point the Bowden tube pops out of the connector.
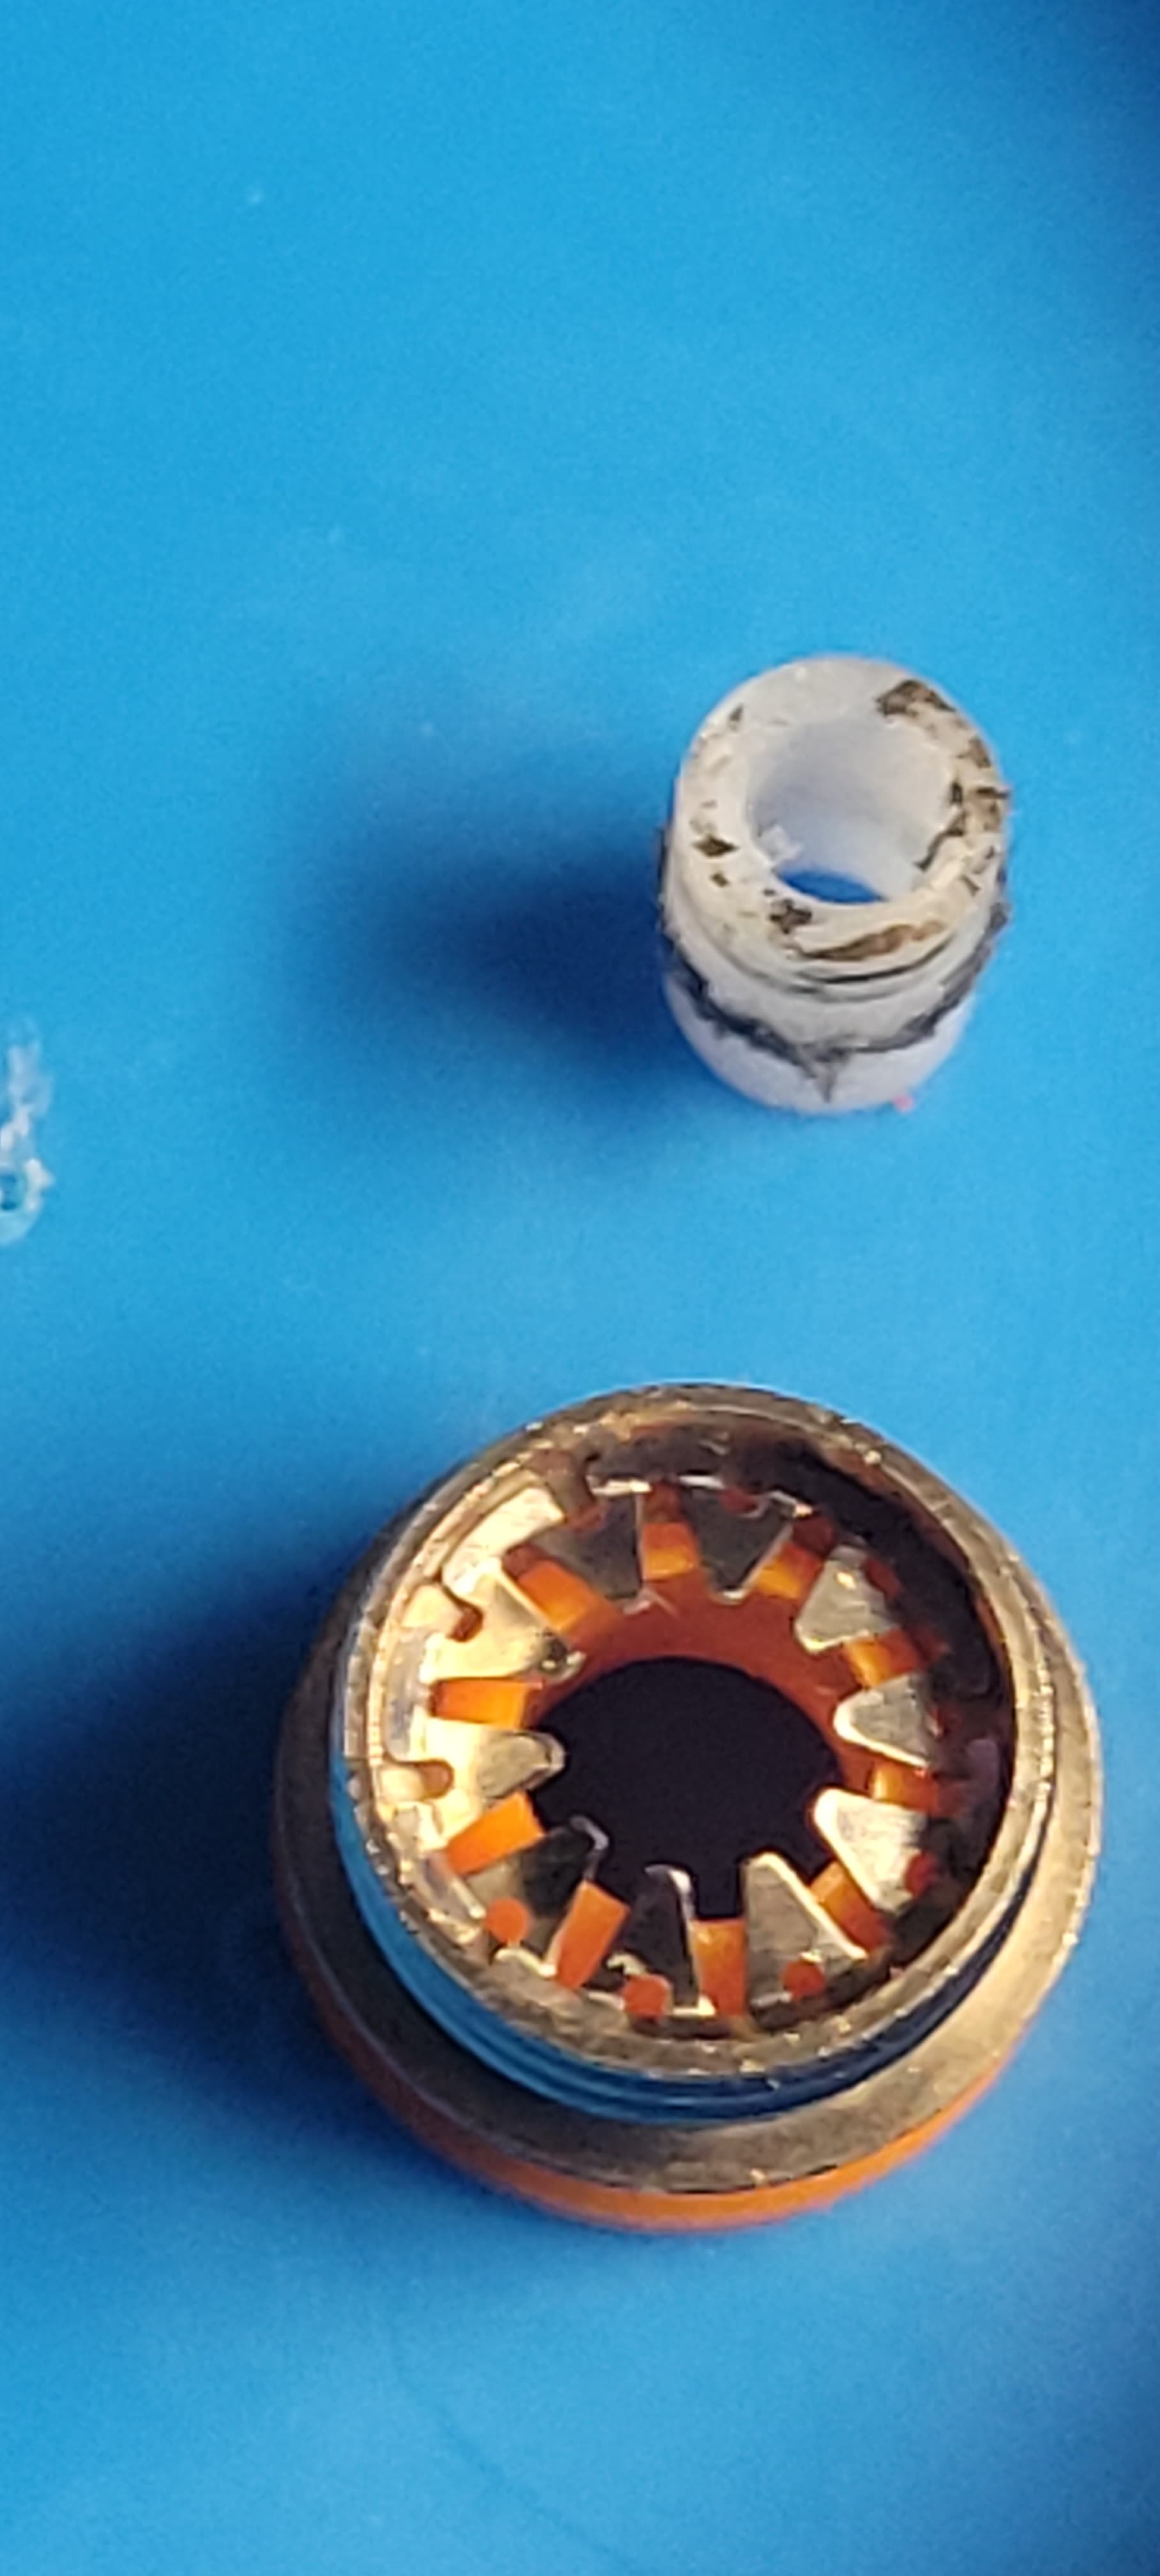
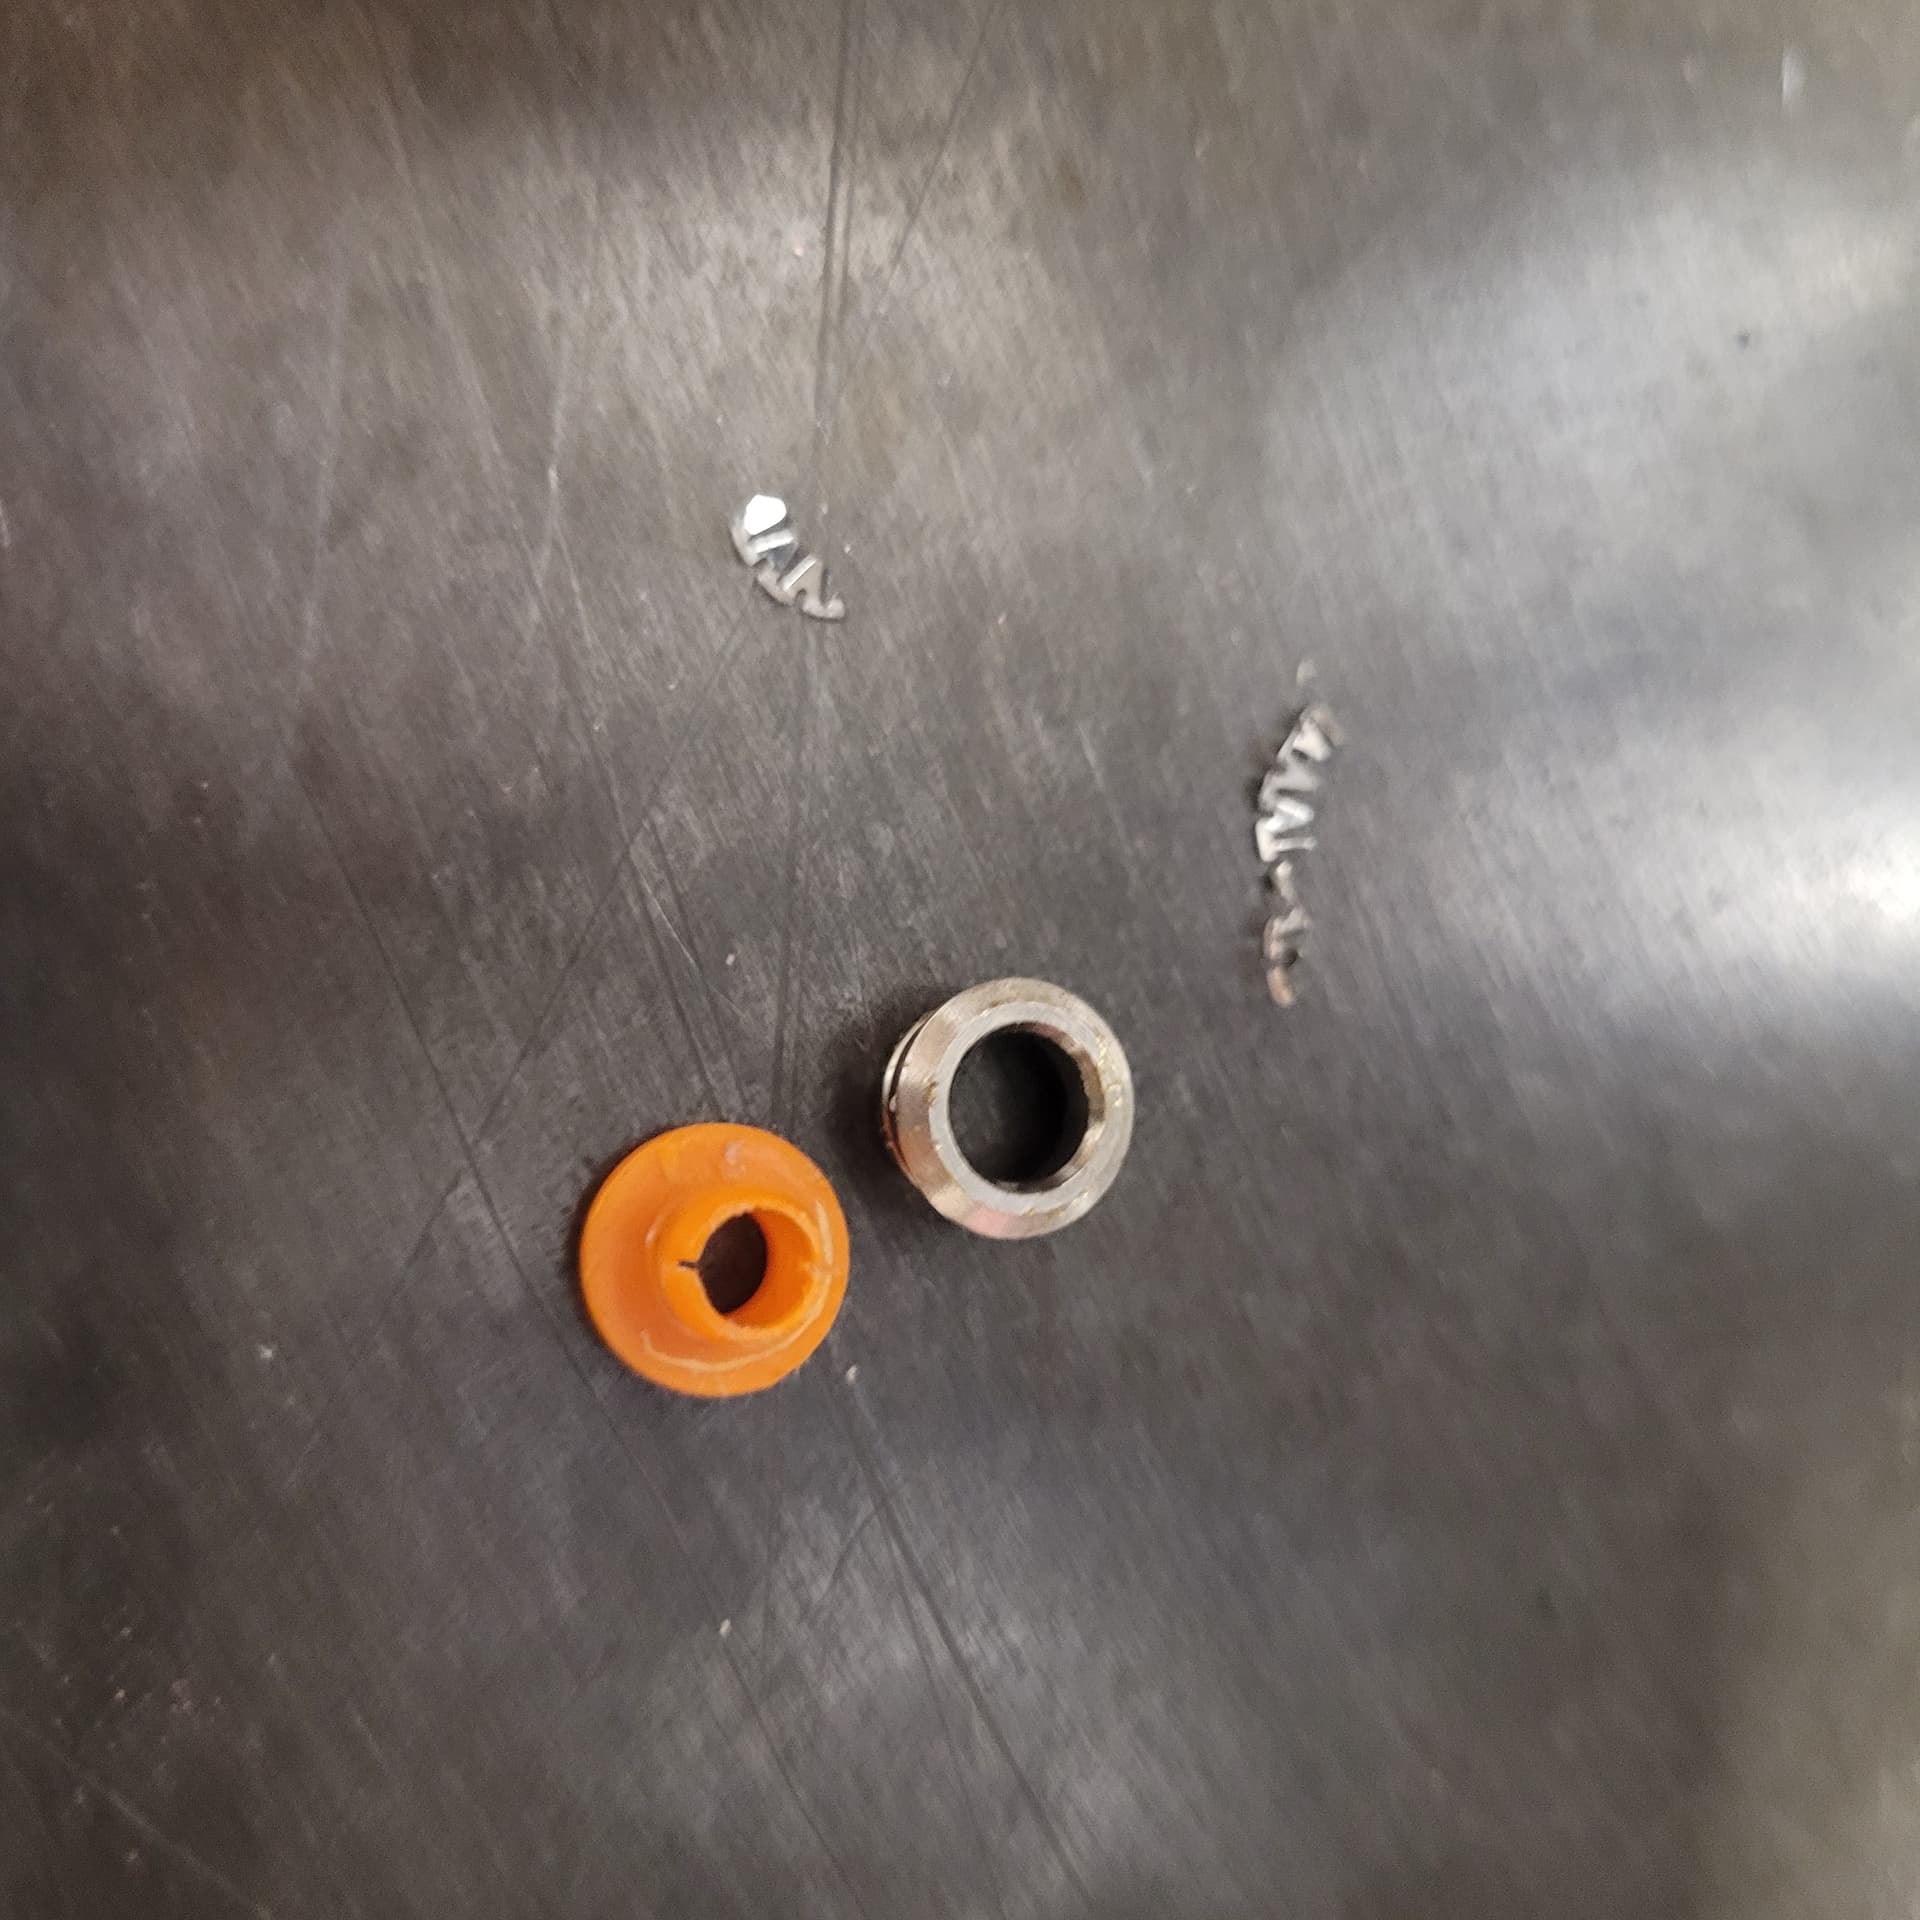
Well my last routine maintenance went rather poorly with less than 30 hours on a refitted extruder fitting the teeth grenaded and I found them in the filament sensor (the small bit at the top of the pic).
Fortunately no permanent damage. All that has been removed and all those spares have been YEETed with extreme prejudice.
I have bought two new sets of gears and front faces as spares as production commitments loom.
I pulled out industrial pneumatic fittings that the PTFE tube goes completely through which I hope helps keeping the shrapnel away from the inside of the extruder.
I do not trust the cobbled on clip “fix” so I got my plastic welder and soldering iron out and proceeded with major surgery. Old and busted out, new hotness installed with loads of plastic CF added to keep the new fitting in place. It did not need to be pretty as the PTFE tube butts up against the existing extruder housing right above the filament sensor. It took less than 15 minutes and I was emboldened as I had a spare extruder incase I messed up this one but it is flawless so far and has over 40 hours on it without an extruder issue printing ABS, ASA and PLA. 95% ABS
The bed though. Swapping from production in ABS to PLA… I am prepping for a graphite bed because the stock one is as stable as a worm in a frying pan. Near full bed ABS prints require a minimum 20 minute 80C heat soak so the bed level from the last one is accurate. Then it prints ABS well. If you try and print PLA without doing a cold relevel it probably will not go well as the bed will be out of level significantly. First layer adhesion and tear off will be a misery. Same thing going the other way. I also had to install a full back baffle to stop air being pulled in by the hot end fan from the exhaust vent and ruining JUST THE UPPER levels of tall ABS prints, spaced banding then hotend topples the lot off the bed with or without brims. THAT was a fun one to figure out. Flawless with the baffle on 300mm plus tall columns.
Back to production…